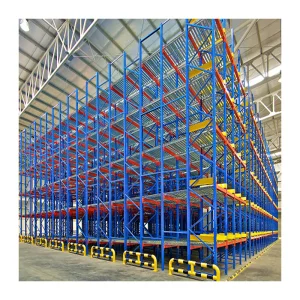
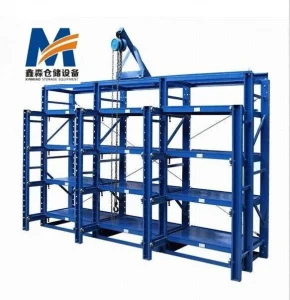
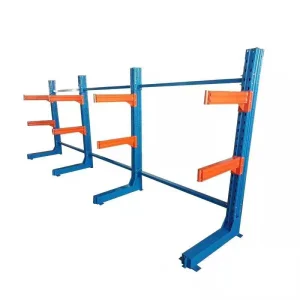
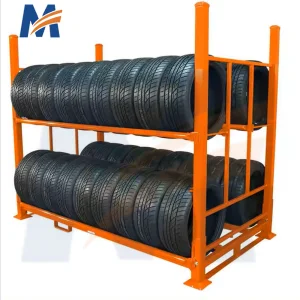
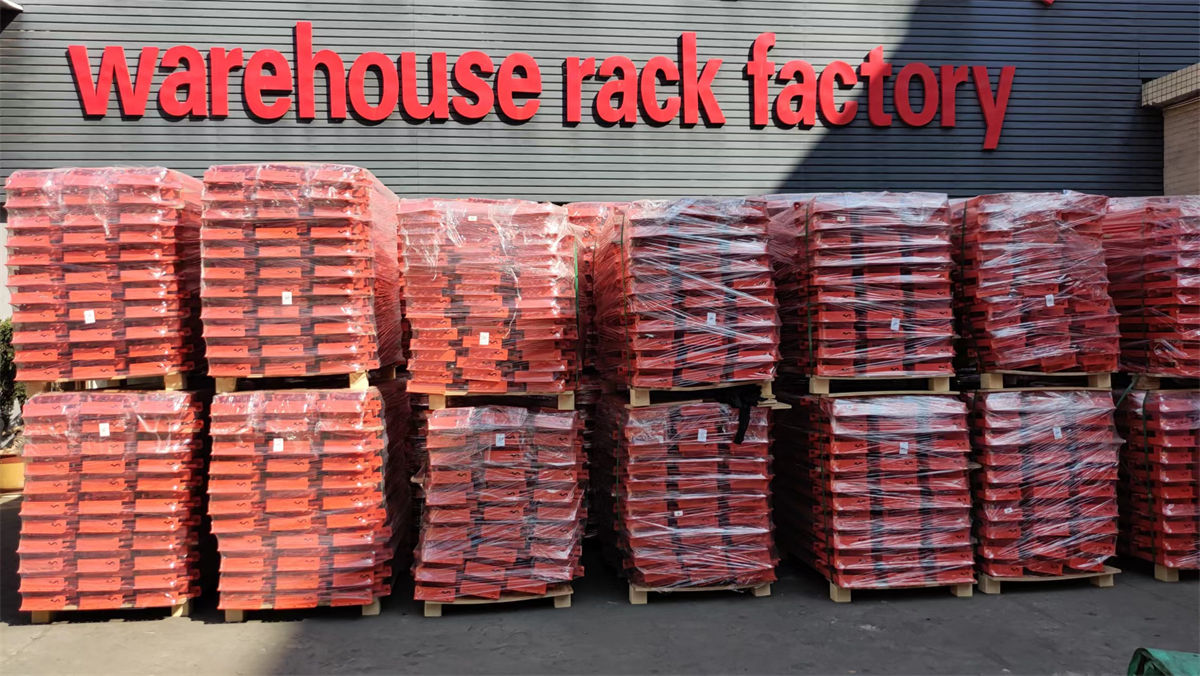
Guangzhou Xinmiao Storage Equipment Co., Ltd. is a professional manufacturer specializing in warehouse storage solutions, industrial racks, and customized shelving systems. Established in 2016, we have accumulated years of experience in designing, manufacturing, and exporting high-quality storage equipment for global customers.
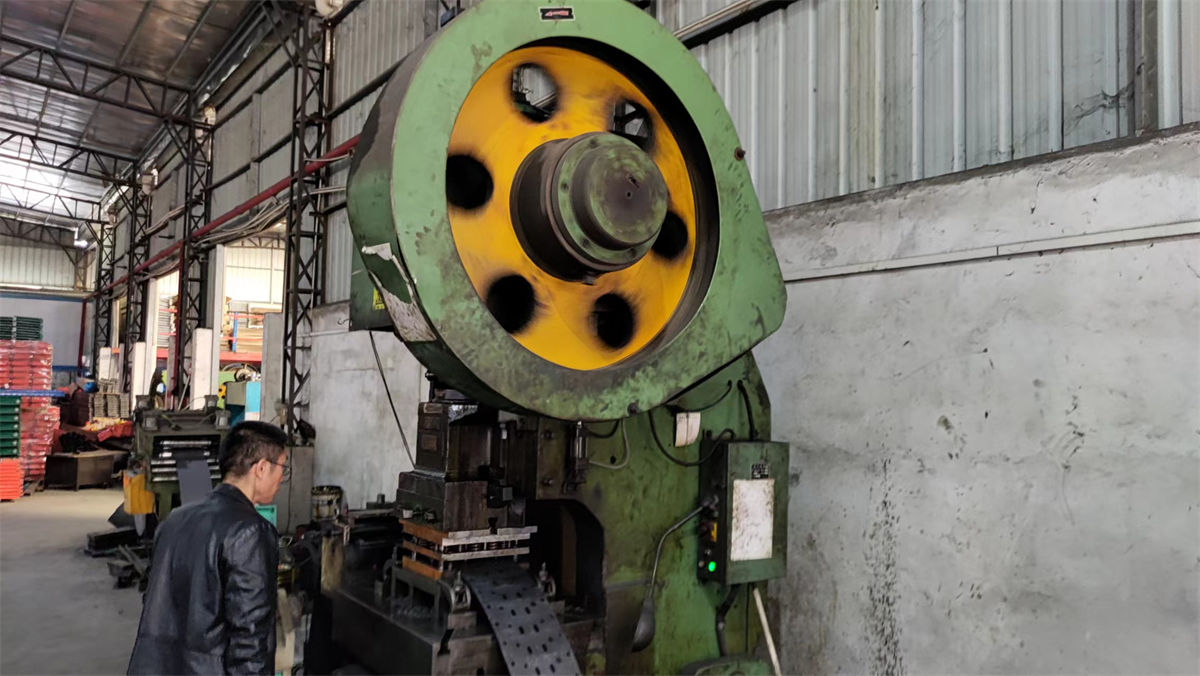
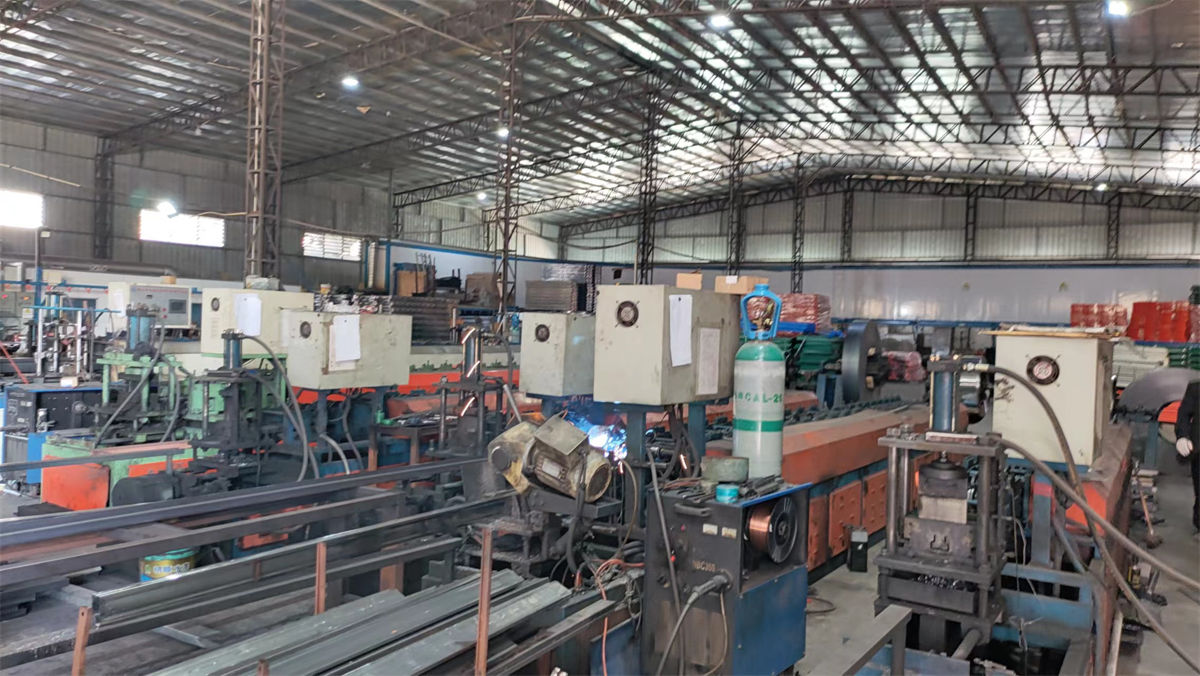
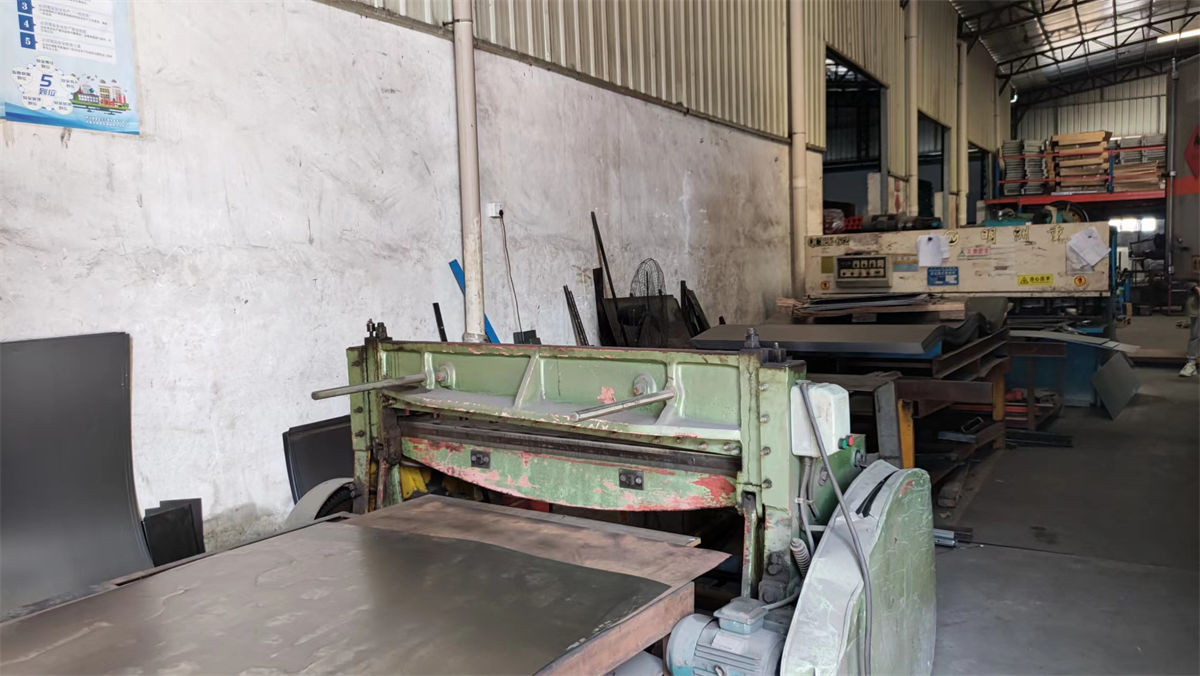
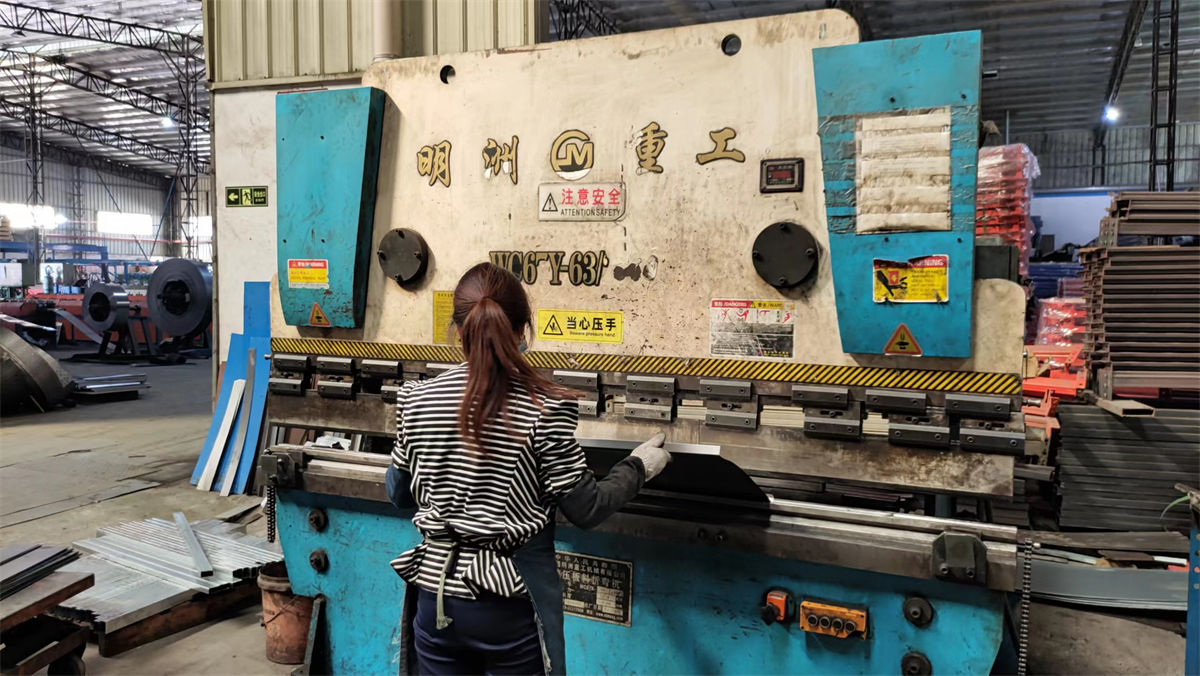
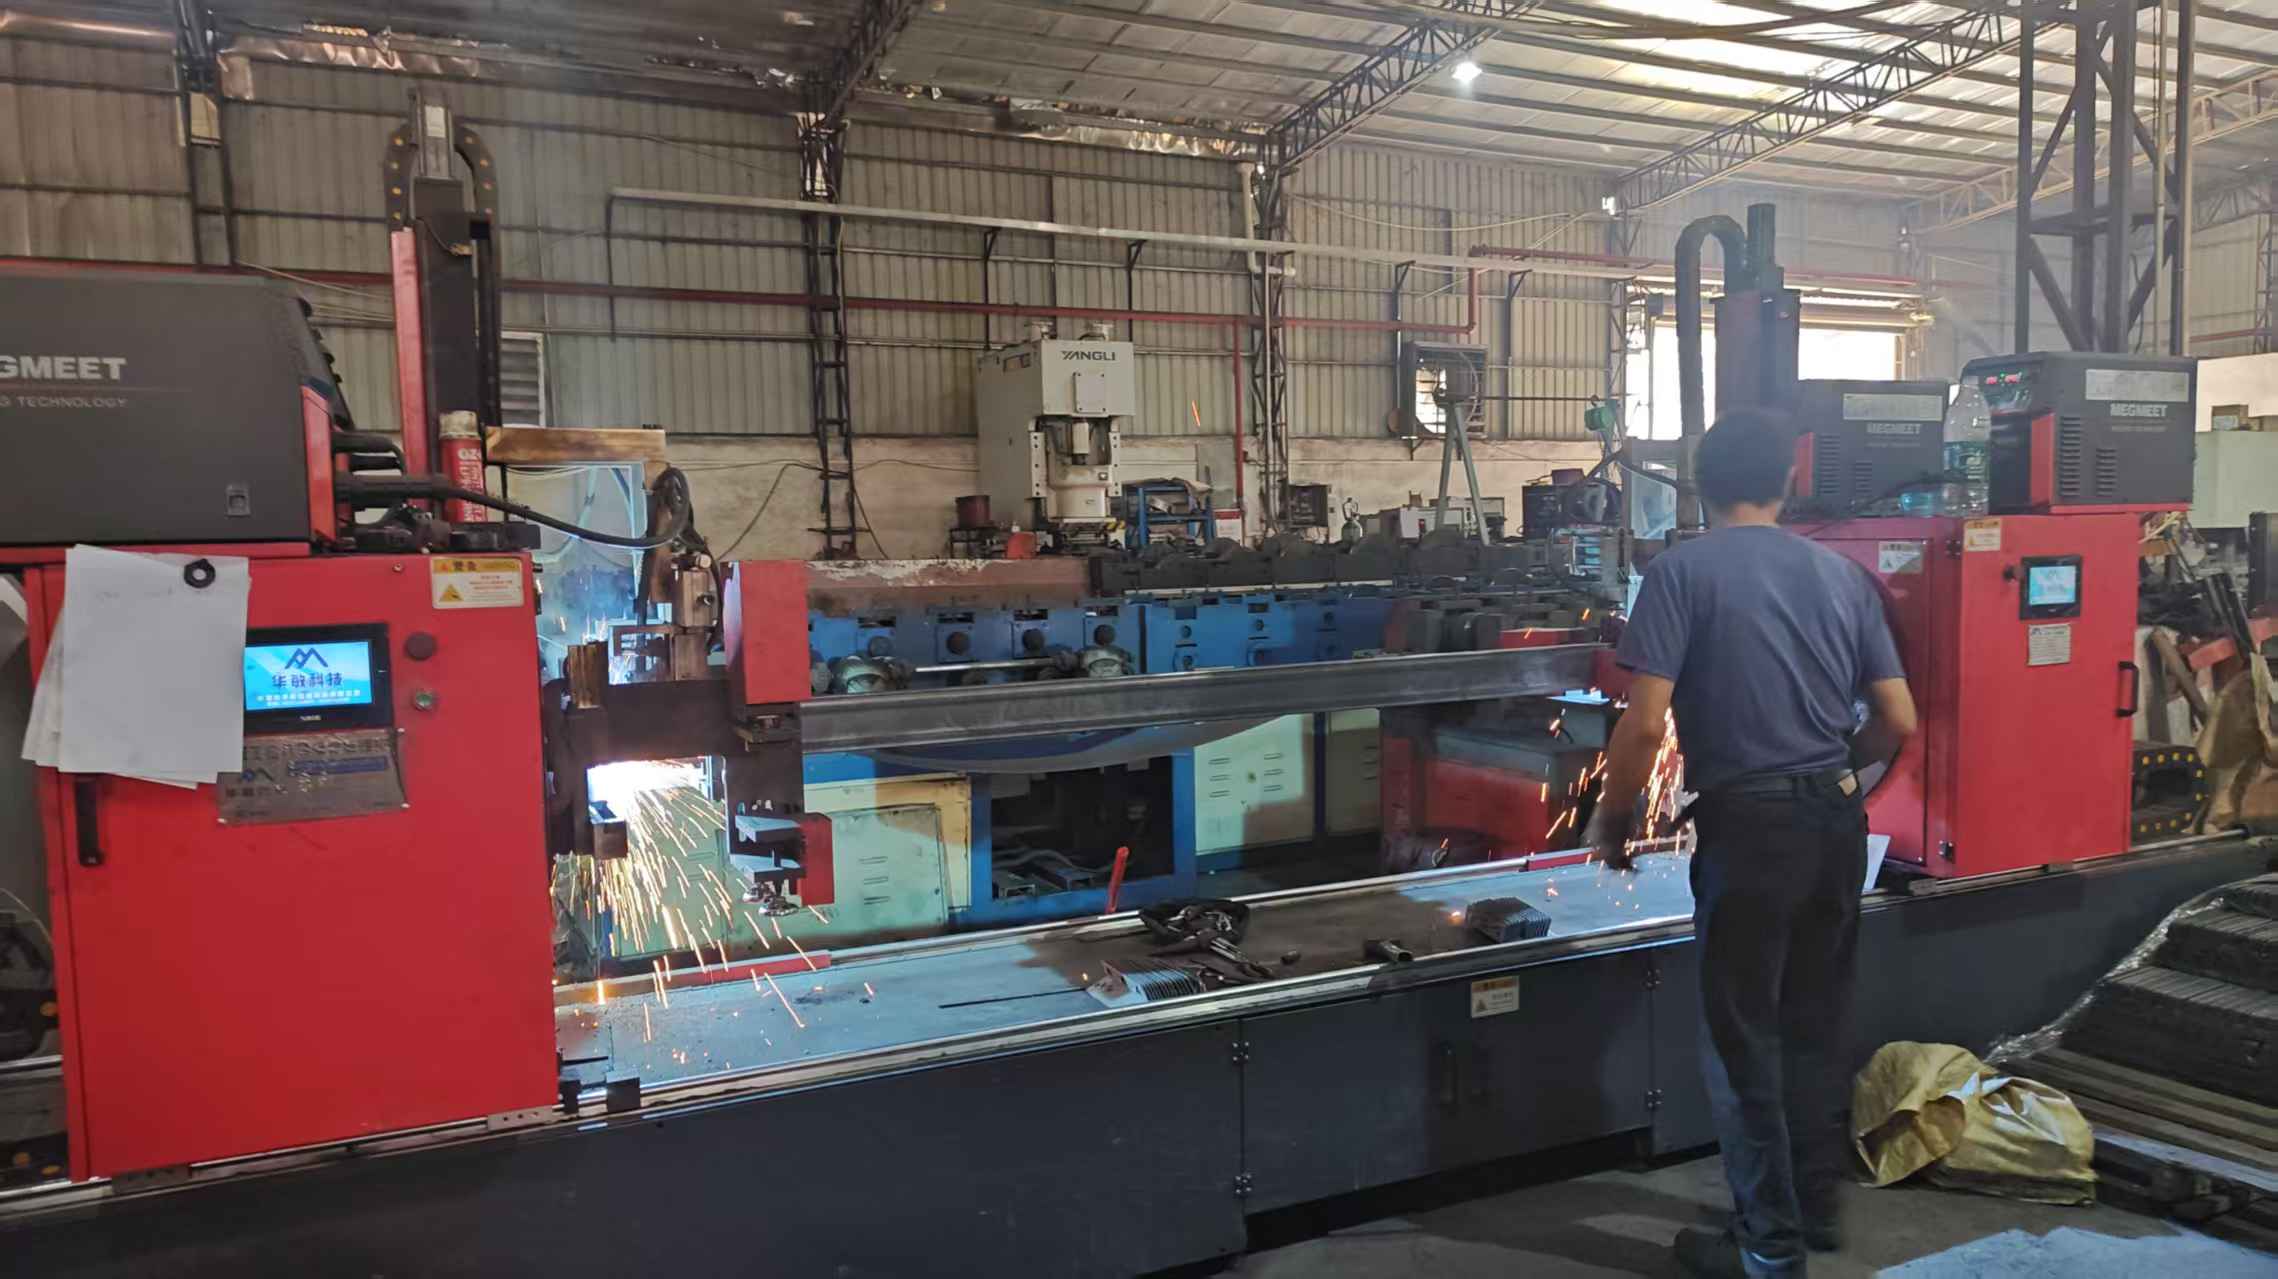
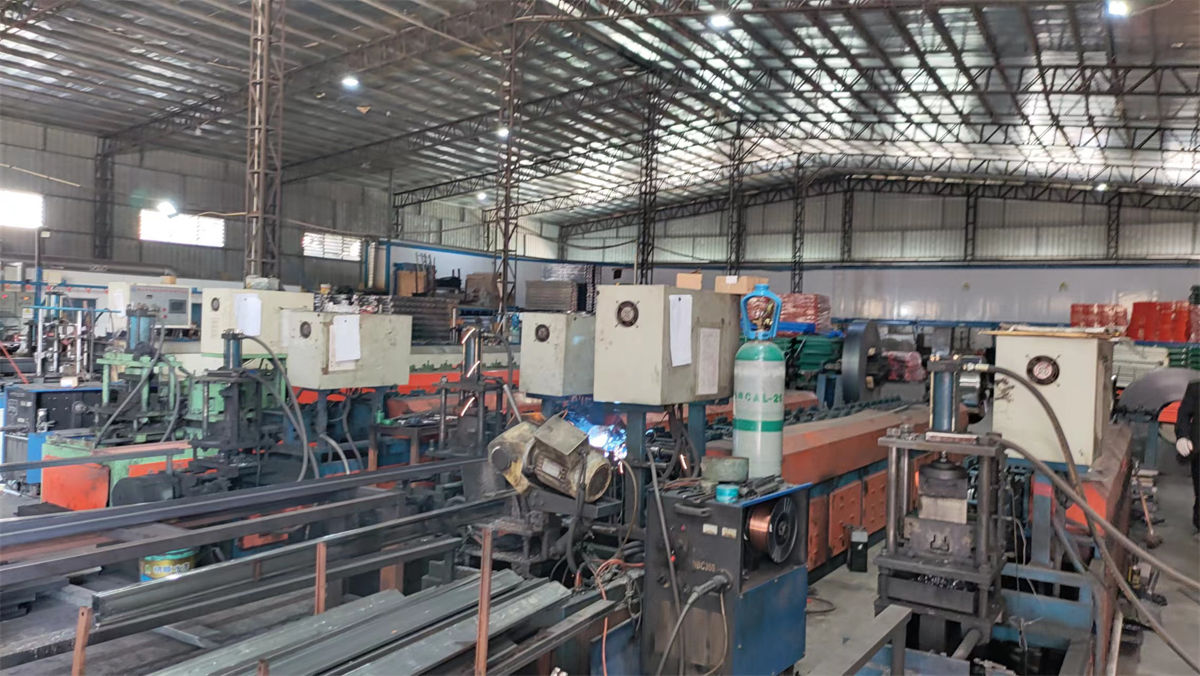
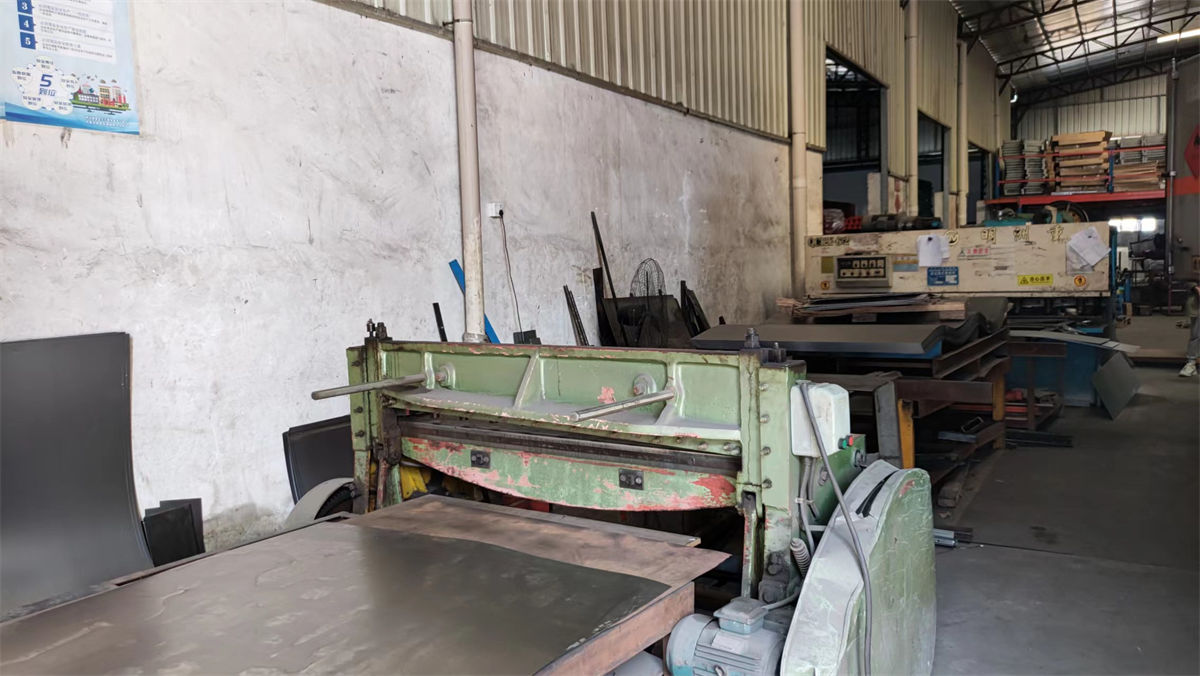
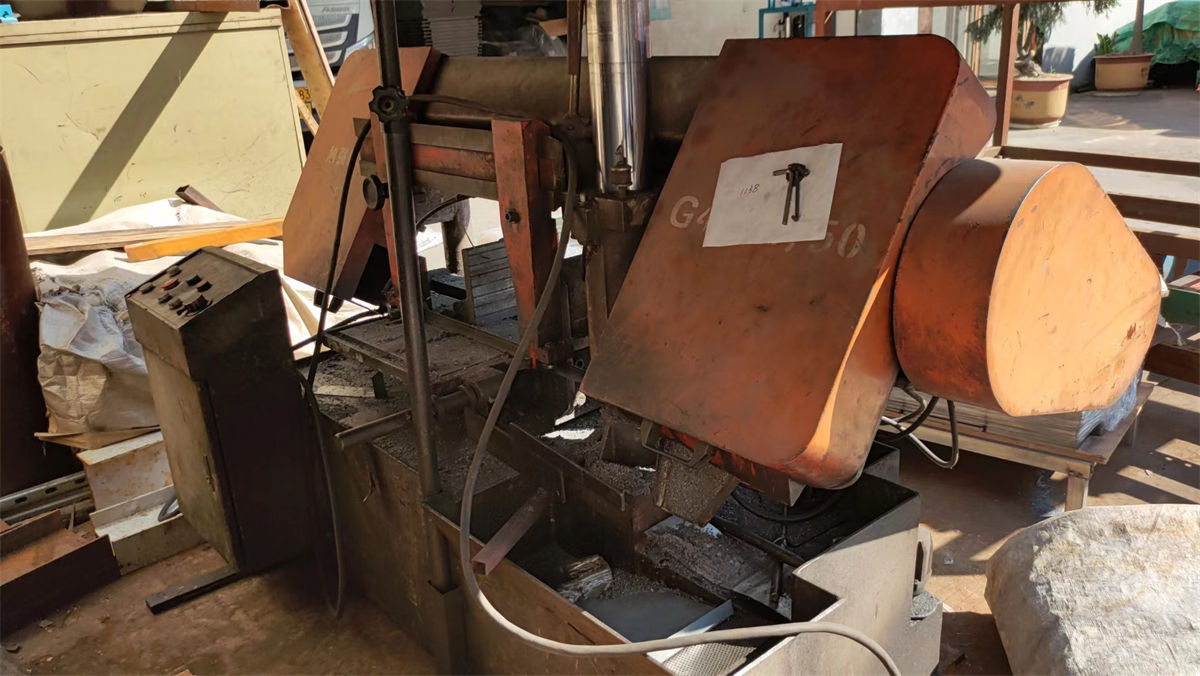
Our factory covers an area of approximately 18,500㎡, equipped with advanced production facilities, automated processing equipment, and a professional quality management system. With an annual export revenue of around USD 12 million, we have built strong partnerships with customers from different industries worldwide. We have 8 years of export experience and 12 years of industry experience, providing reliable storage solutions for warehouses, factories, logistics centers, retail stores, and distribution facilities.
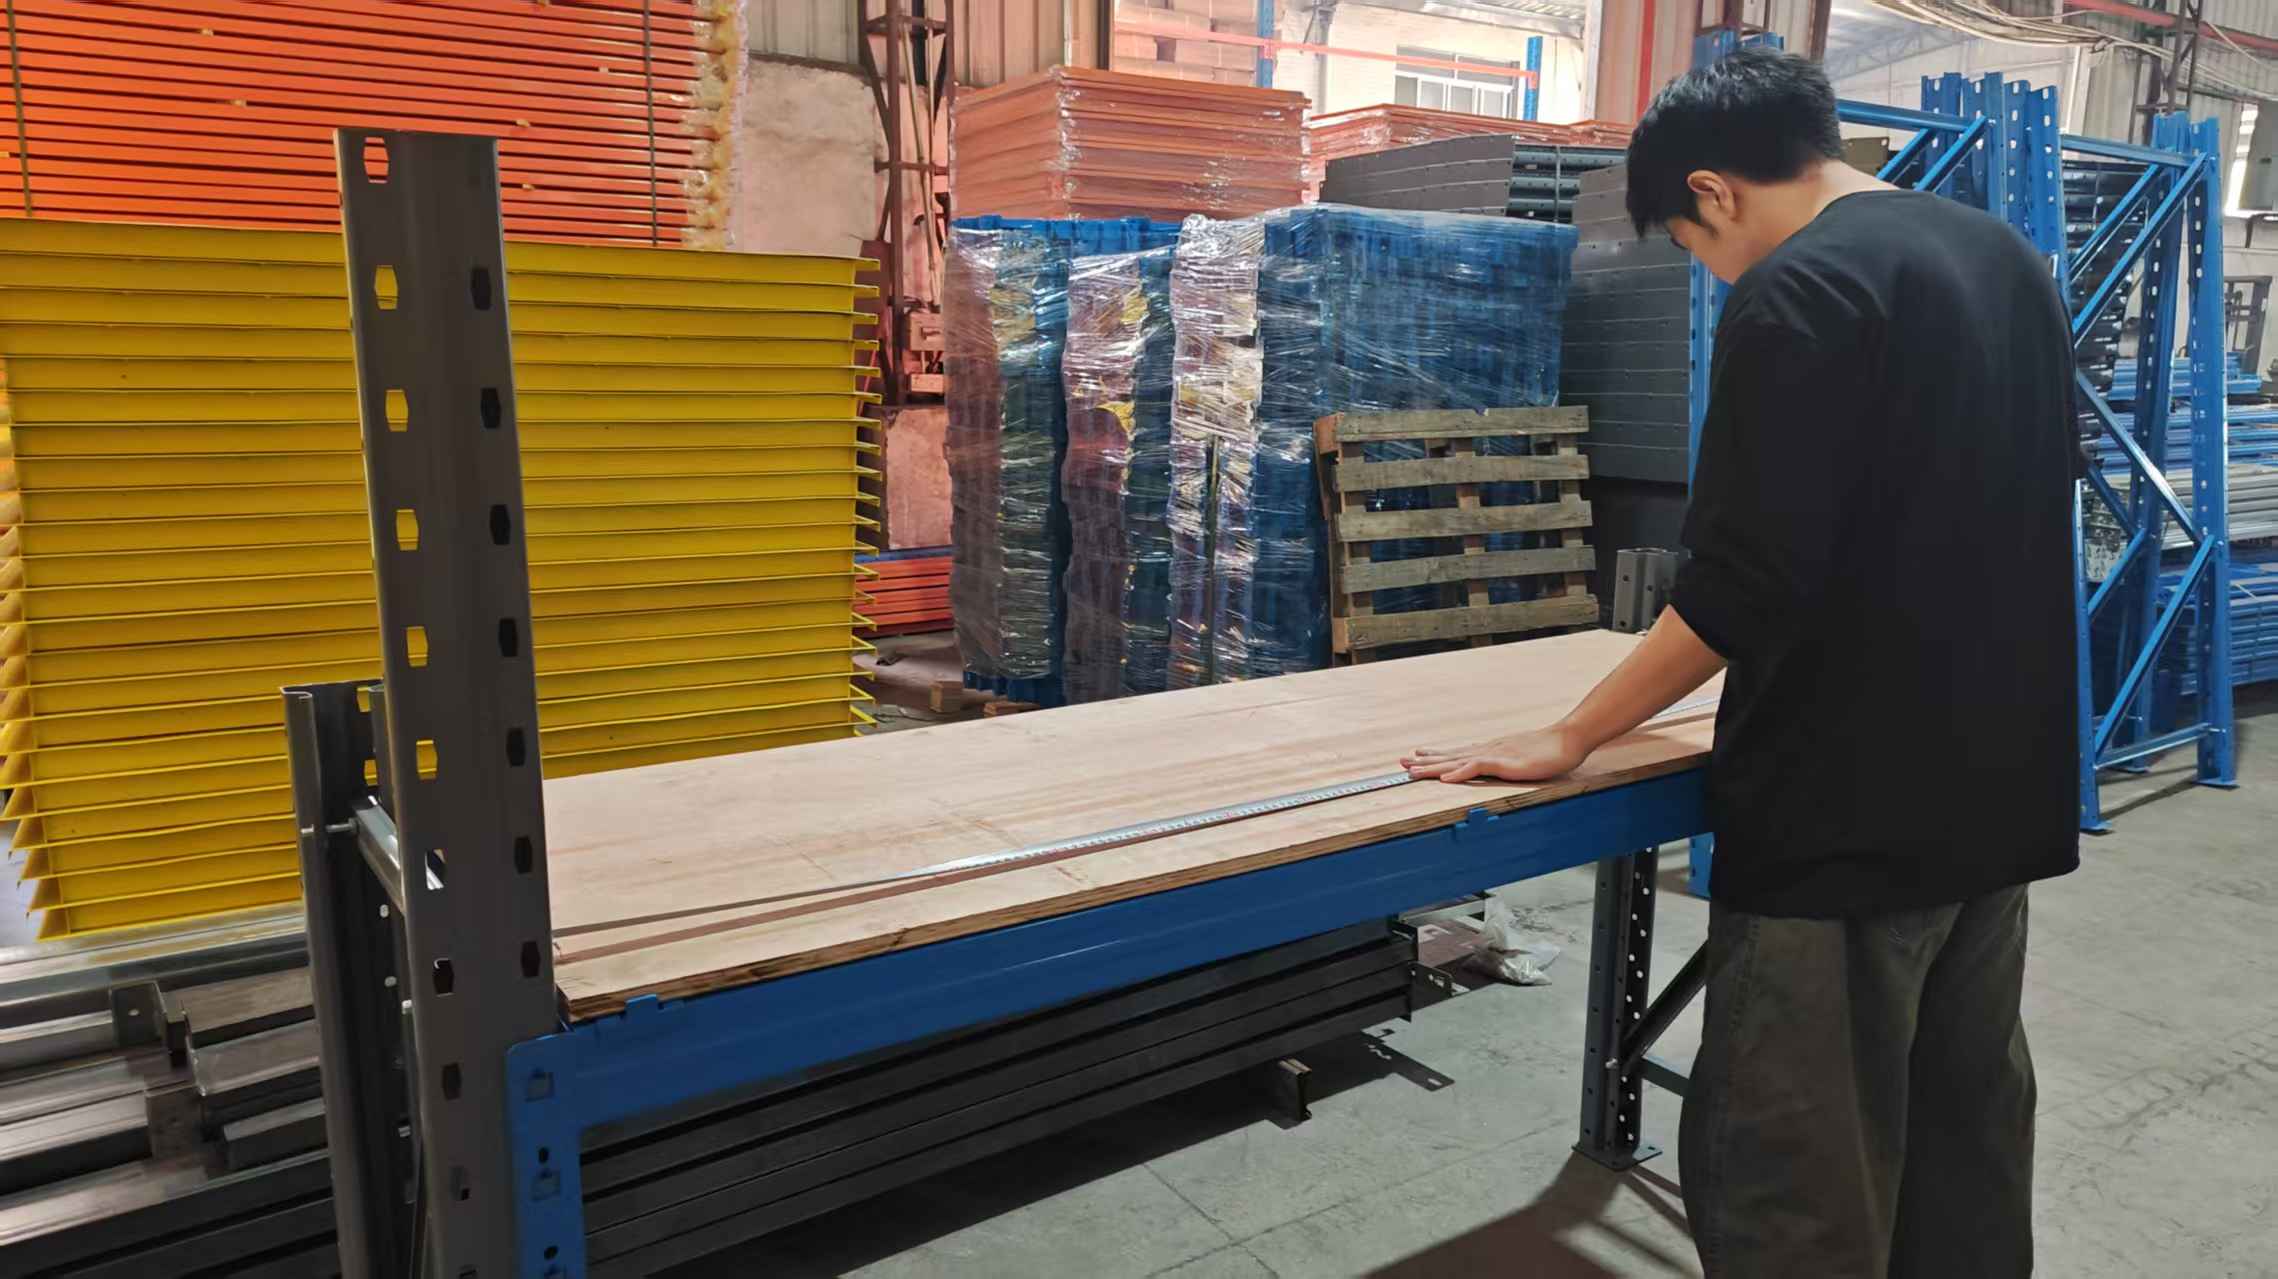
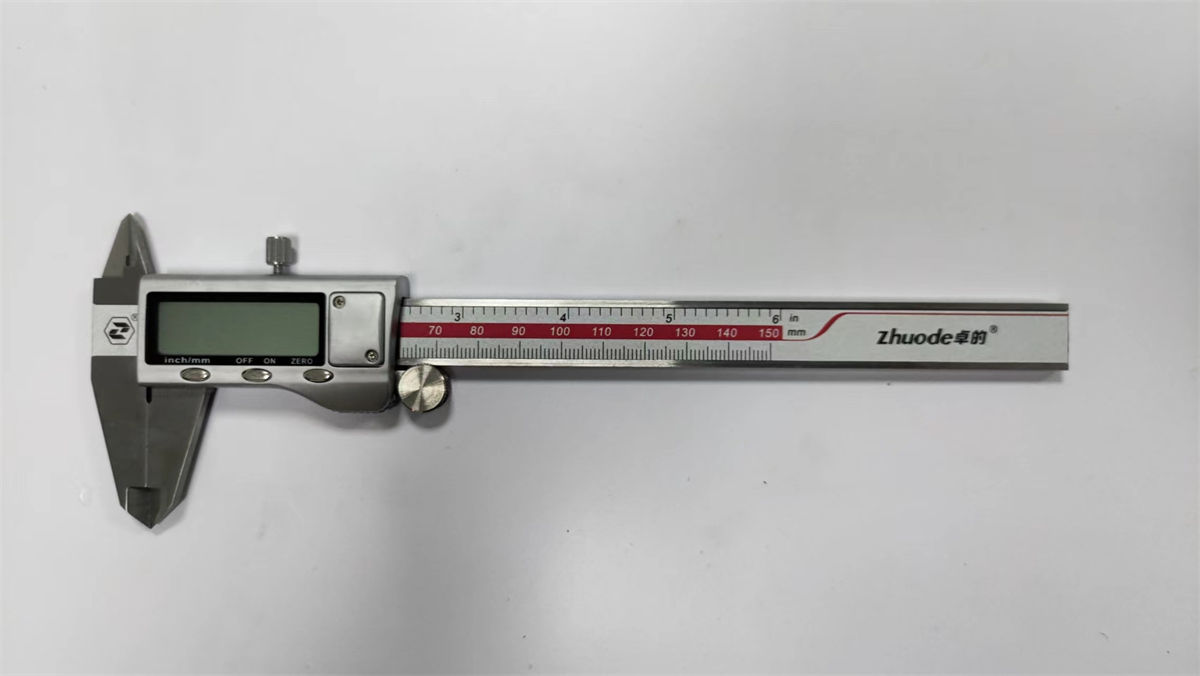
To ensure consistent product quality, we implement strict quality control procedures throughout the entire production process. Our quality inspection system includes raw material testing, welding inspection, dimensional measurement, surface coating inspection, load-bearing tests, and finished product evaluation. We use advanced inspection methods such as laser measurement, load testing equipment, and visual quality inspection to guarantee product safety and durability. Our dedicated quality control team consists of 45 professional inspectors.
With extensive international trade experience, Xinmiao Storage Equipment has developed a stable global supply chain network and maintains cooperation with more than 850 suppliers and partners. Our products are exported to major markets including North America, Europe, Southeast Asia, the Middle East, and Australia. Our main customers include logistics companies, manufacturing enterprises, e-commerce warehouses, wholesalers, distributors, and retail chains.
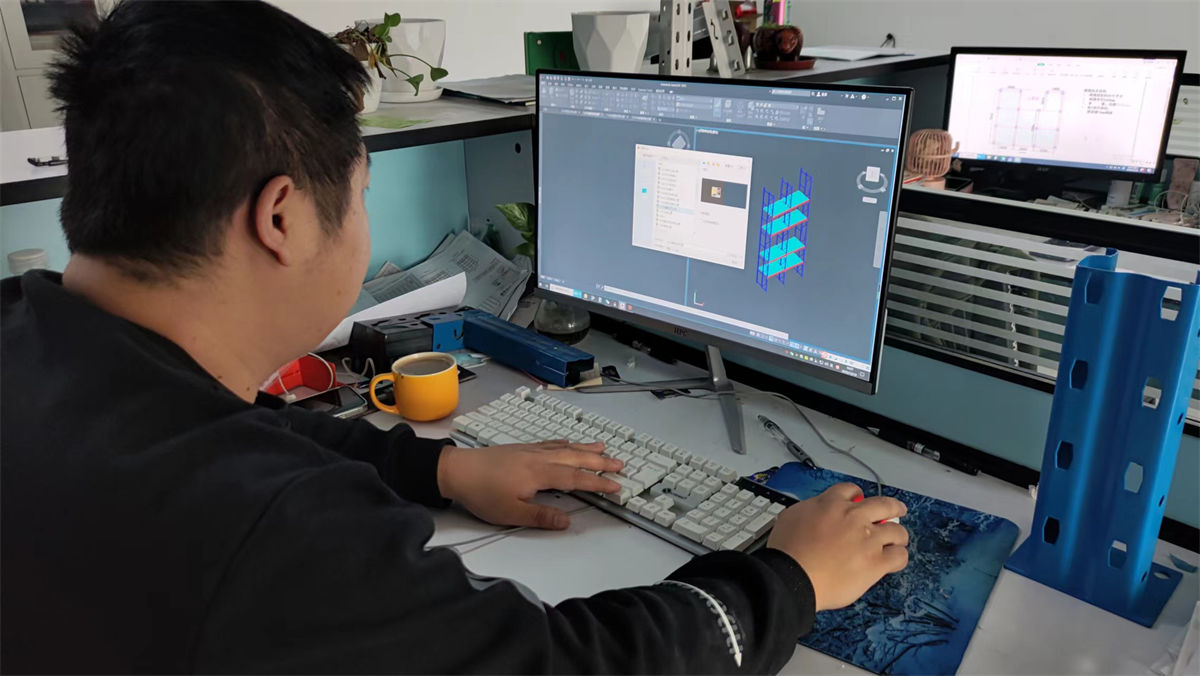
We have strong research and development capabilities supported by 68 experienced R&D engineers. Our team focuses on innovative storage technologies, space optimization solutions, and product improvements. We provide comprehensive customization services, including OEM/ODM solutions, customized dimensions, load capacity design, color options, structural modifications, and complete warehouse planning services.
Every year, we continue to invest in product innovation and market development. In the past year, we launched 126 new storage products to meet the evolving needs of global customers. Our professional engineering team works closely with clients to develop efficient, safe, and cost-effective storage solutions.
Guangzhou Xinmiao Storage Equipment Co., Ltd. is committed to delivering high-quality warehouse racking systems, professional service, and long-term value for customers worldwide. We welcome global partners to cooperate with us and build smarter storage solutions together.
In today’s hyper-competitive global supply chain environment, inventory management systems (IMS) have evolved far beyond basic digital spreadsheets and legacy warehouse management software. Modern industrial operations require an intricate synergy between cutting-edge software ecosystems and robust physical storage hardware infrastructure—such as heavy-duty racking, automated shelving, and modular mezzanine floors. As international e-commerce surges, supply chain resilience, real-time tracking, and optimal space utilization have become core pillars for manufacturing enterprises and distribution hubs worldwide.
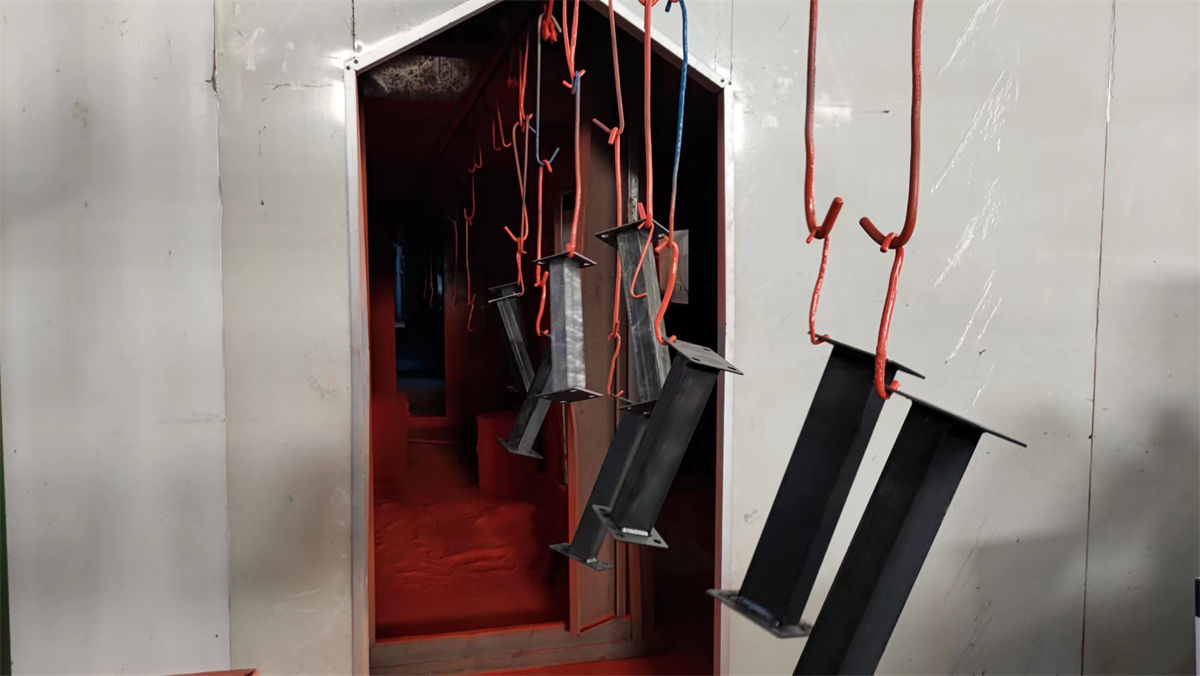
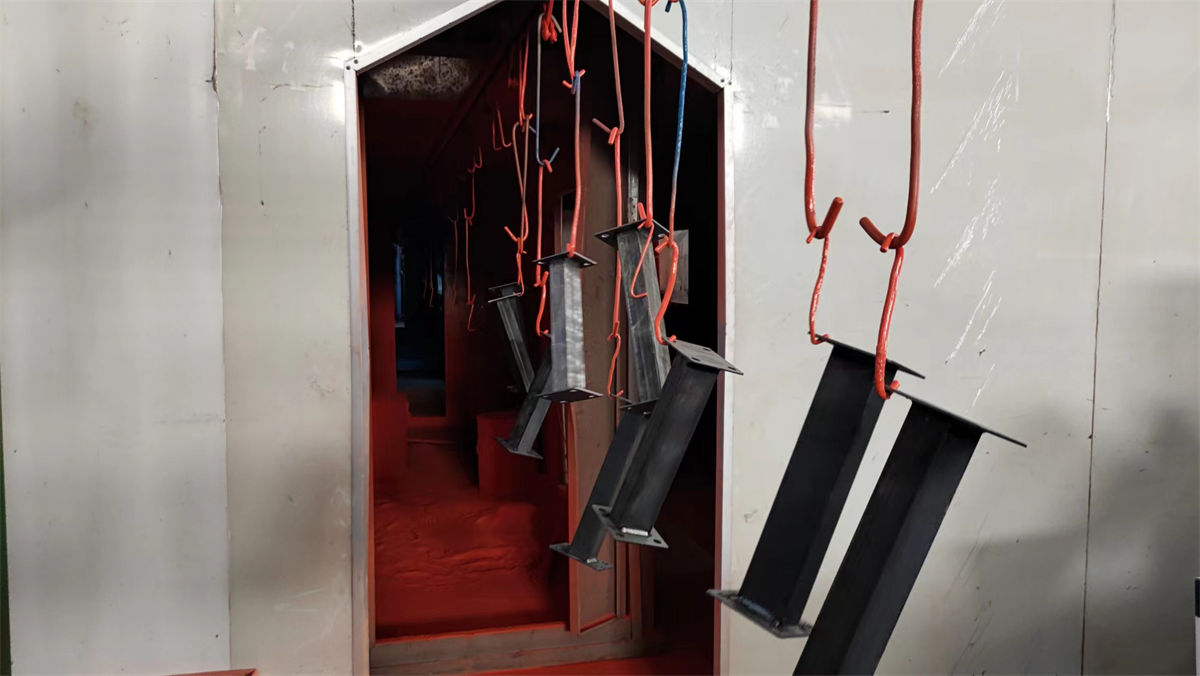
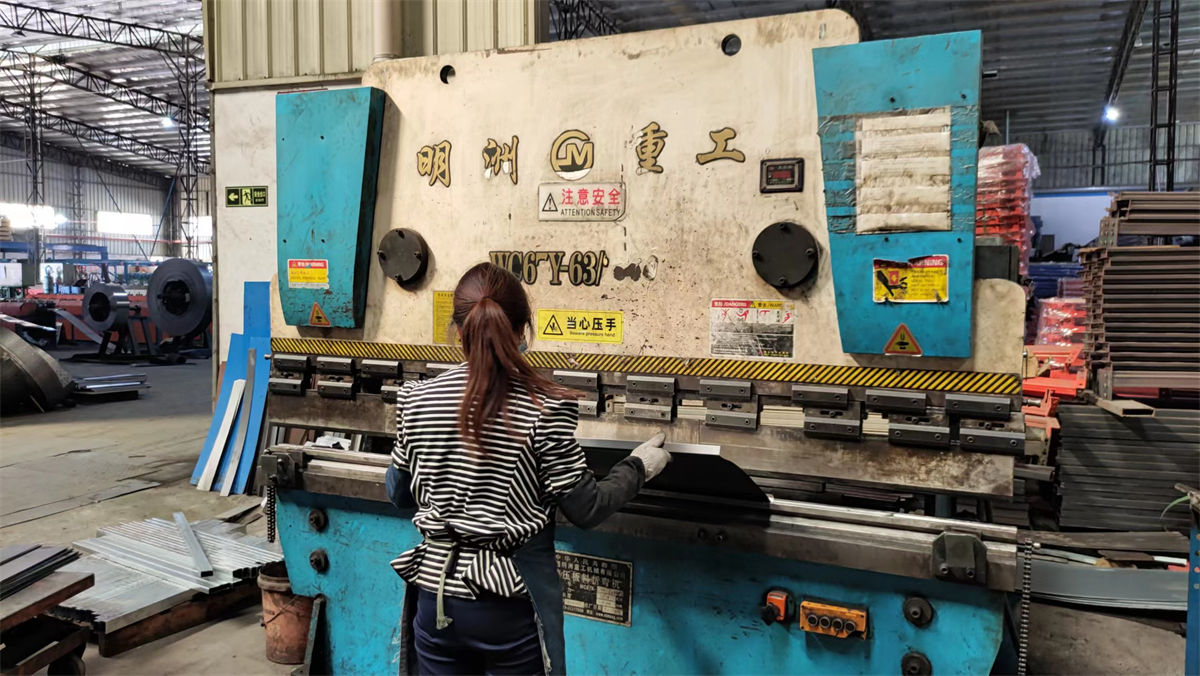
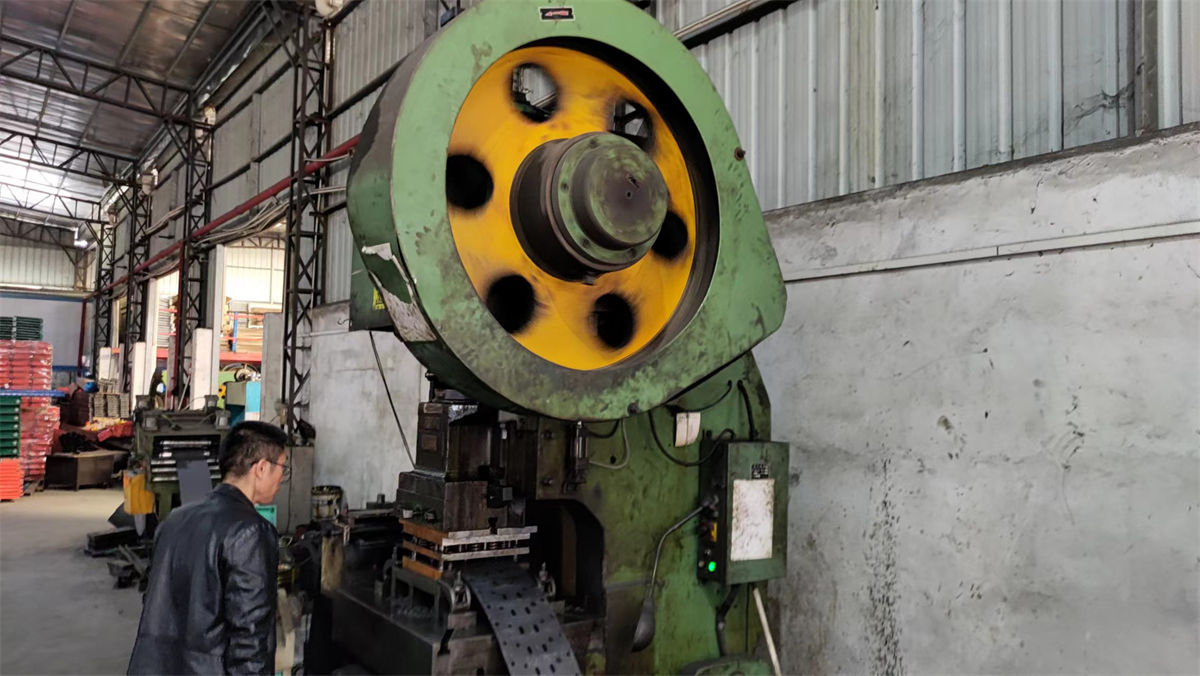
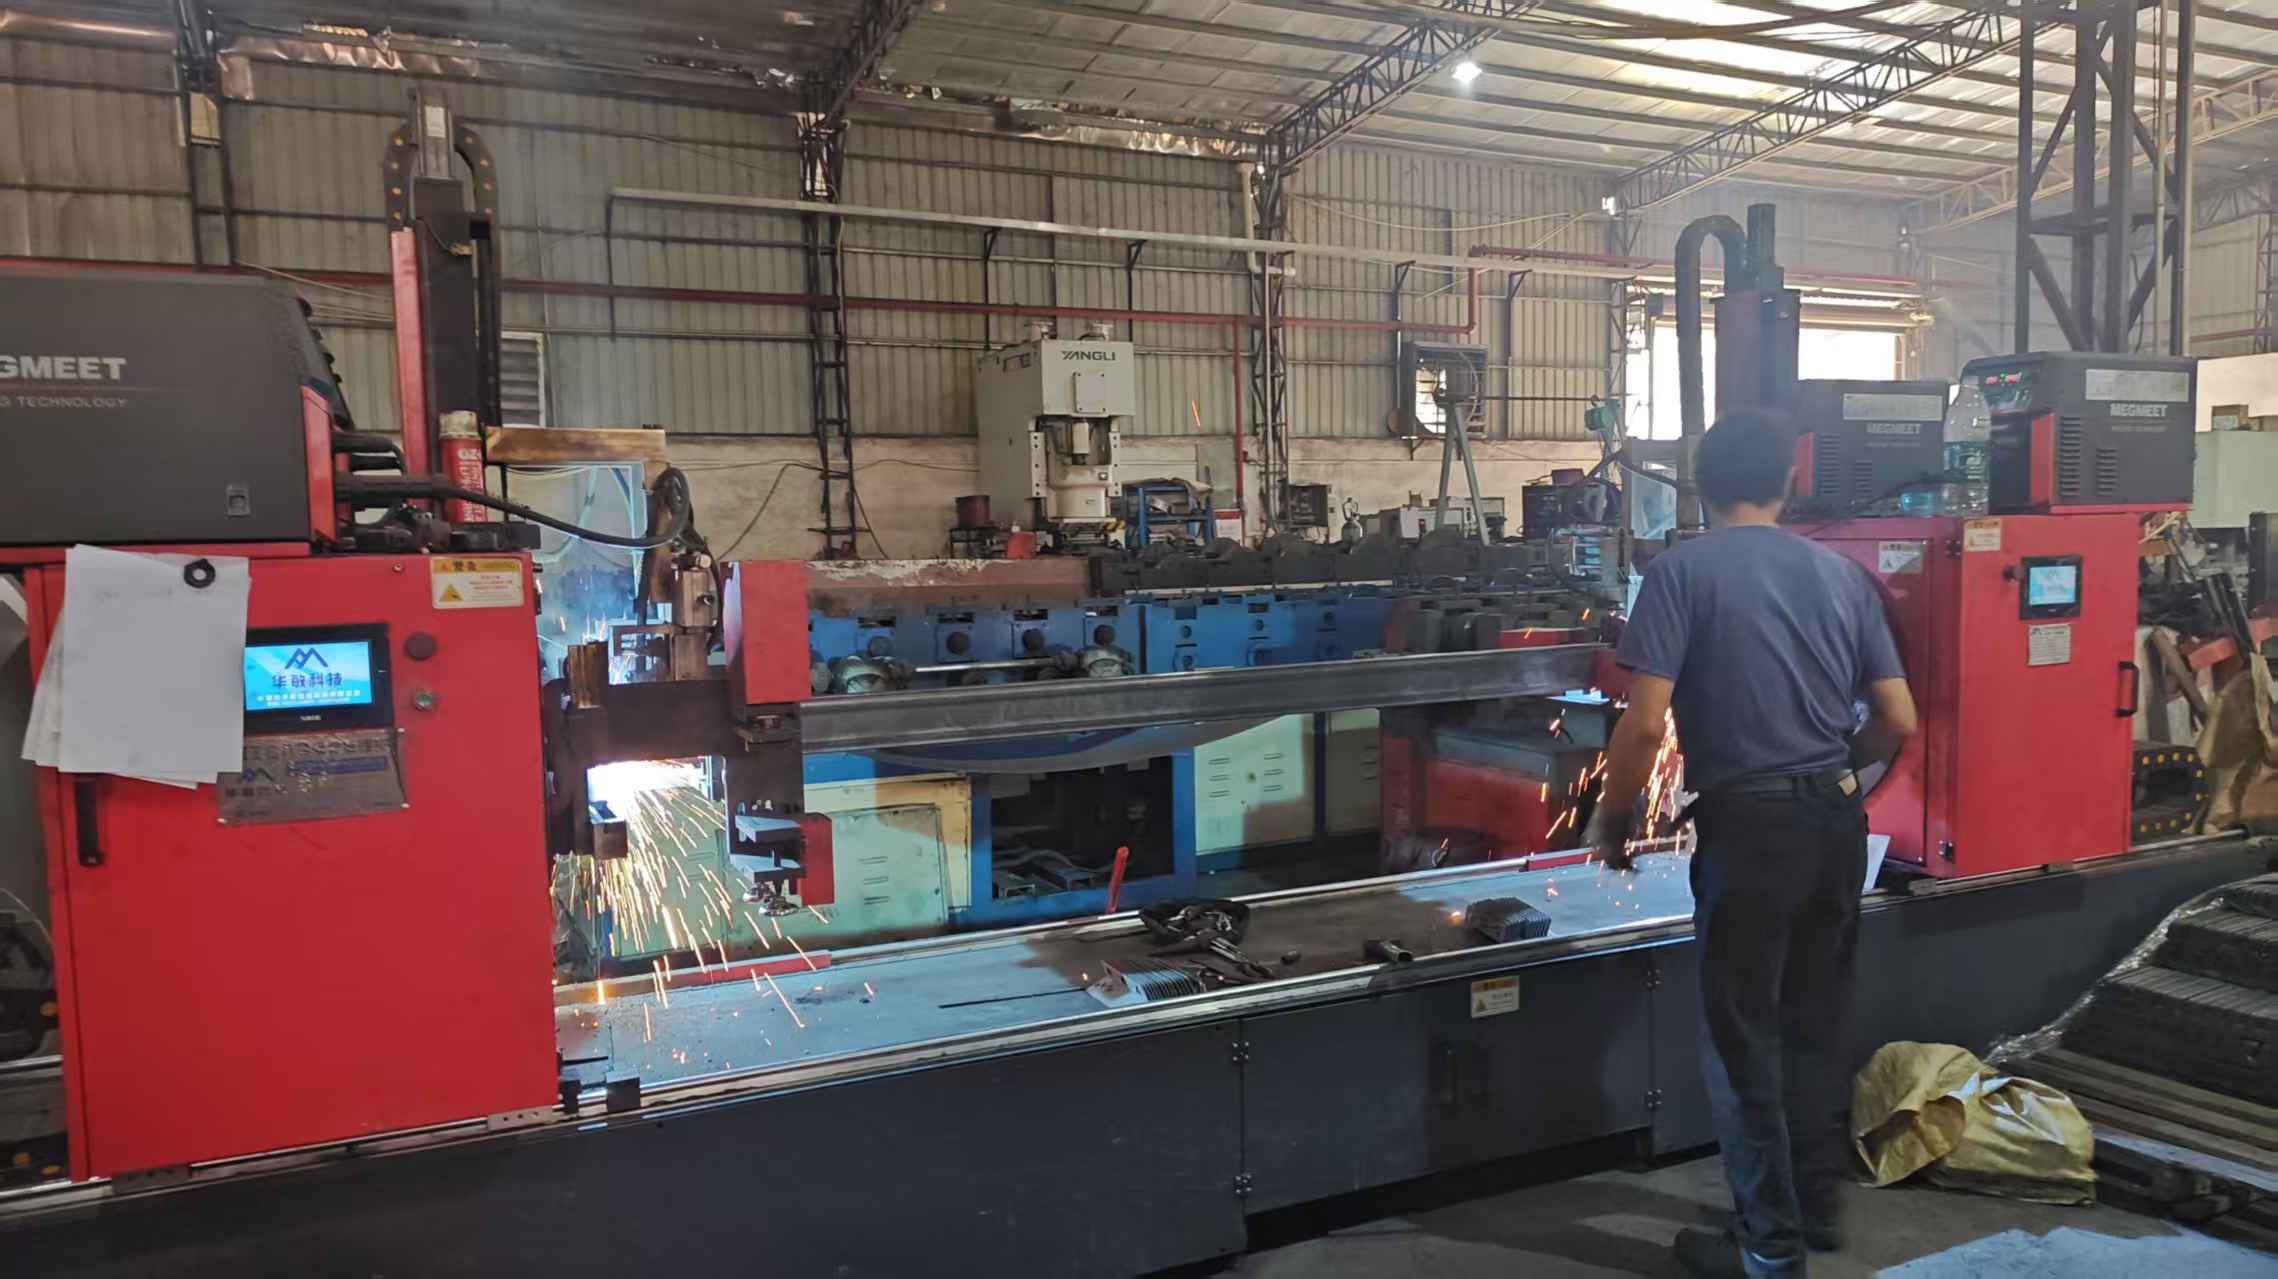
China remains the global epicenter for industrial storage manufacturing. Factories in industrial hubs like Guangzhou leverage advanced automated production lines, laser cutting technology, precise robotic welding, and high-efficiency powder coating systems to deliver exceptional structural integrity and load capacity. By integrating stringent quality control protocols—ranging from raw material tensile testing to rigorous load-bearing evaluations—Chinese manufacturers provide international buyers with certified, durable, and highly cost-effective storage solutions that comply with global safety standards.
Warehouse storage and inventory systems must be customized to address distinct regional and sector-specific requirements:
Looking forward, the integration of IoT sensors, automated guided vehicles (AGVs), and smart inventory tracking will redefine warehouse architecture. Manufacturers are focusing on eco-friendly production processes, recyclable steel materials, and energy-efficient powder coating lines. Suppliers that combine digital adaptability with superior physical engineering will continue to lead the global export market.
Chinese factories offer an unmatched combination of advanced manufacturing infrastructure, cost-efficiency, strict quality control procedures, and extensive export experience. Companies like Guangzhou Xinmiao Storage Equipment provide robust engineering support, custom OEM/ODM solutions, and high-capacity production lines capable of fulfilling large international orders efficiently.
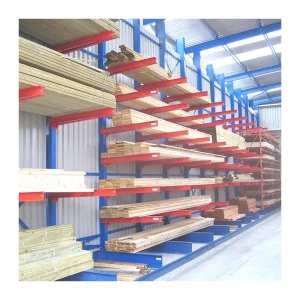
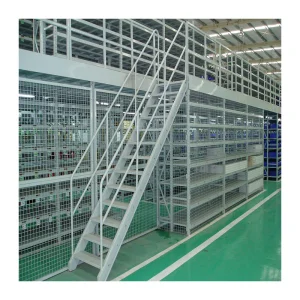
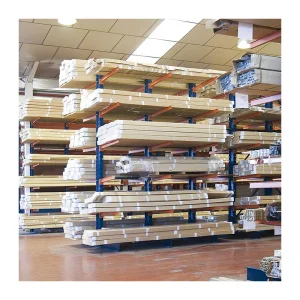
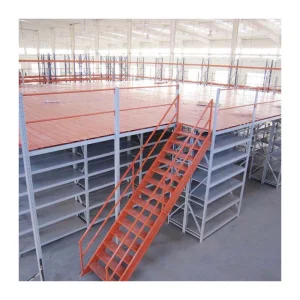
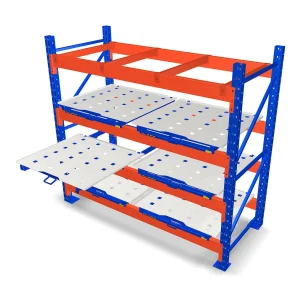
The selection depends on your inventory turnover rate, product dimensions, weight capacity, and available warehouse vertical space. For high-density storage, gravity racking or double-deep racks are ideal. For long or bulky items, cantilever racks are recommended, while multi-tier mezzanine floors maximize vertical height.
Ensure that the manufacturer implements rigorous inspection protocols such as raw material testing, welding inspection, and load-bearing evaluations. Look for international compliance certifications such as CE certification, ISO quality management standards, and adherence to structural safety codes.
Yes. Professional manufacturers offer comprehensive customization services, including custom dimensions, specialized load capacities, tailored color coatings, and full CAD warehouse layout planning to optimize your operational workflow.
 Xinmiao Storage