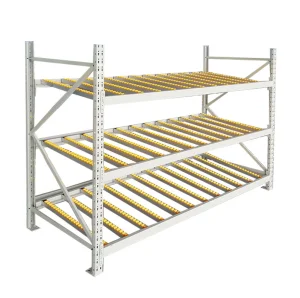

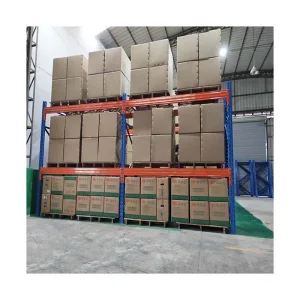
In the contemporary global logistics ecosystem, supply chain velocity and warehouse cube utilization dictate enterprise competitiveness. As a leading China Wholesale Gravity Flow Racking Factory & Suppliers, Guangzhou Xinmiao Storage Equipment Co., Ltd. delivers high-density storage frameworks designed around the FIFO (First-In, First-Out) principle. Gravity flow racks—also known as live pallet racking—utilize inclined roller tracks powered entirely by gravity. Pallets loaded at the high end glide smoothly on durable roller beds to the picking face, ensuring automated stock rotation without electrical energy consumption.
Equipped with precision-engineered braking rollers, speed controllers, and heavy-duty steel tracks that govern descent velocity, preventing impact damage to sensitive cargo.
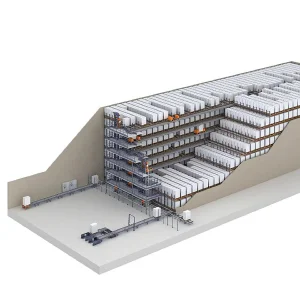
Dramatically reduces forklift aisles by merging multiple pallet depths into a single lane, capturing up to 85% more volumetric storage capacity compared to traditional selective racking.
Constructed from premium high-tensile structural steel, finished with high-durability powder coating resistant to corrosion, abrasion, and harsh industrial environments.
Guangzhou Xinmiao Storage Equipment Co., Ltd. is a professional manufacturer specializing in warehouse storage solutions, industrial racks, and customized shelving systems. Established in 2016, we have accumulated years of experience in designing, manufacturing, and exporting high-quality storage equipment for global customers.
Our factory covers an area of approximately 18,500㎡, equipped with advanced production facilities, automated processing equipment, and a professional quality management system. With an annual export revenue of around USD 12 million, we have built strong partnerships with customers from different industries worldwide. We have 8 years of export experience and 12 years of industry experience, providing reliable storage solutions for warehouses, factories, logistics centers, retail stores, and distribution facilities.
To ensure consistent product quality, we implement strict quality control procedures throughout the entire production process. Our quality inspection system includes raw material testing, welding inspection, dimensional measurement, surface coating inspection, load-bearing tests, and finished product evaluation. We use advanced inspection methods such as laser measurement, load testing equipment, and visual quality inspection to guarantee product safety and durability. Our dedicated quality control team consists of 45 professional inspectors.
With extensive international trade experience, Xinmiao Storage Equipment has developed a stable global supply chain network and maintains cooperation with more than 850 suppliers and partners. Our products are exported to major markets including North America, Europe, Southeast Asia, the Middle East, and Australia. Our main customers include logistics companies, manufacturing enterprises, e-commerce warehouses, wholesalers, distributors, and retail chains.
We have strong research and development capabilities supported by 68 experienced R&D engineers. Our team focuses on innovative storage technologies, space optimization solutions, and product improvements. We provide comprehensive customization services, including OEM/ODM solutions, customized dimensions, load capacity design, color options, structural modifications, and complete warehouse planning services.
Every year, we continue to invest in product innovation and market development. In the past year, we launched 126 new storage products to meet the evolving needs of global customers. Our professional engineering team works closely with clients to develop efficient, safe, and cost-effective storage solutions.
Guangzhou Xinmiao Storage Equipment Co., Ltd. is committed to delivering high-quality warehouse racking systems, professional service, and long-term value for customers worldwide. We welcome global partners to cooperate with us and build smarter storage solutions together.
State-of-the-art machinery and rigorous quality control protocols ensuring zero-defect production standards.
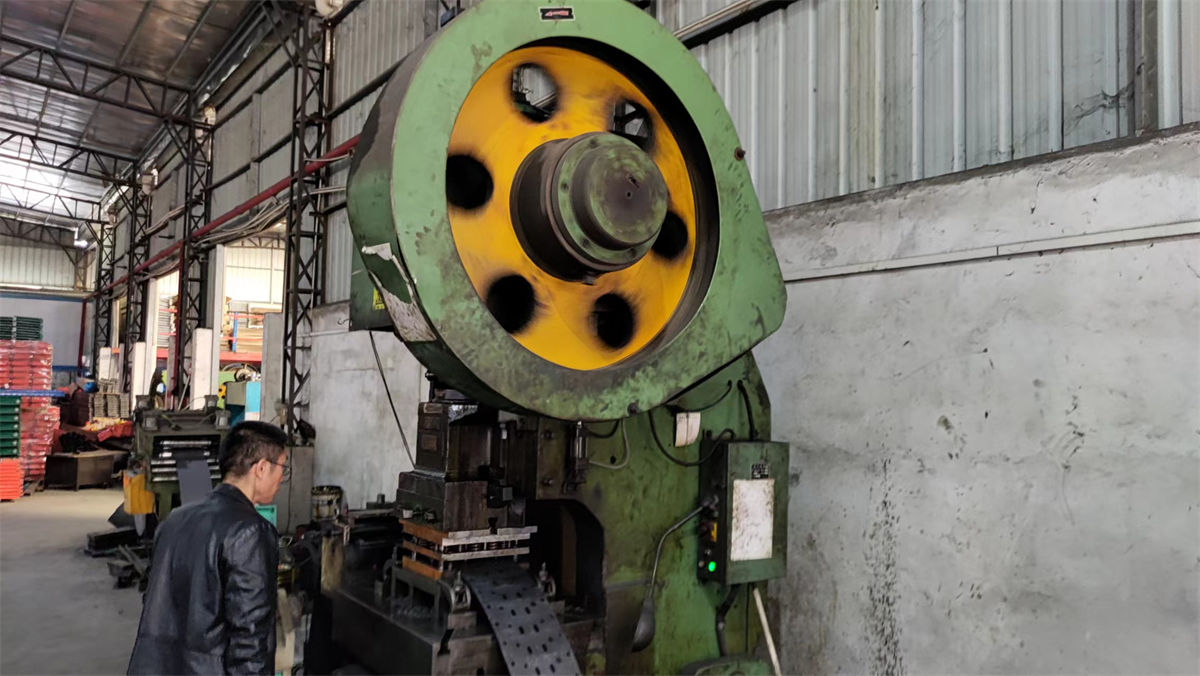
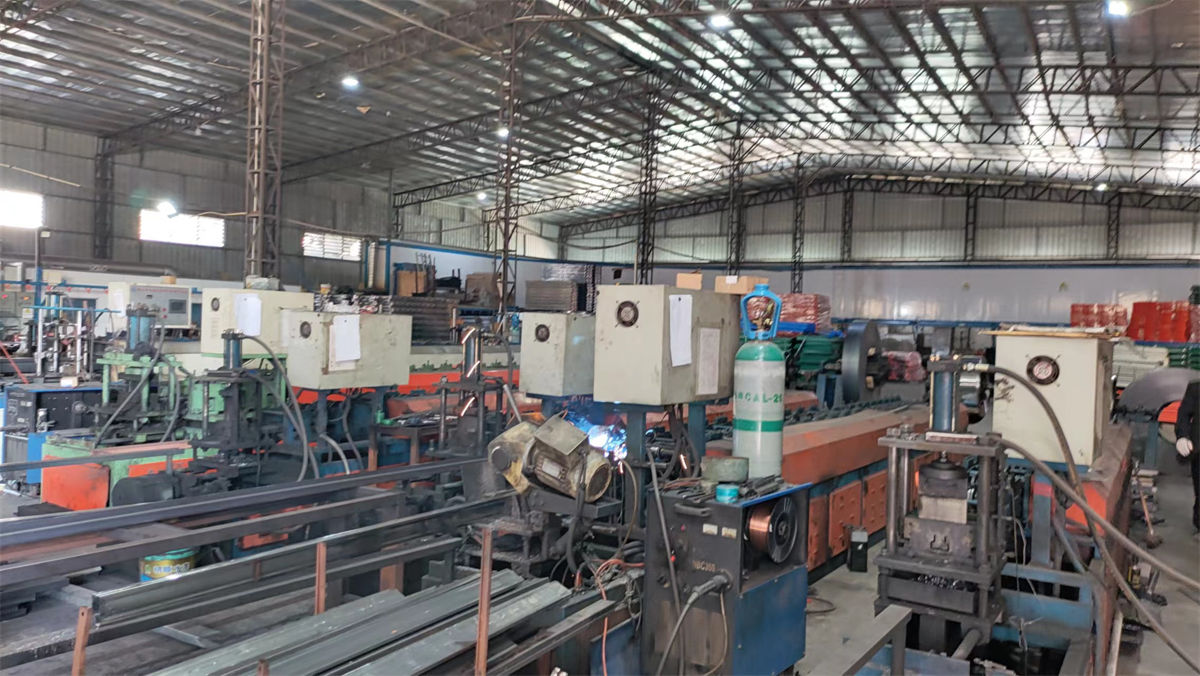
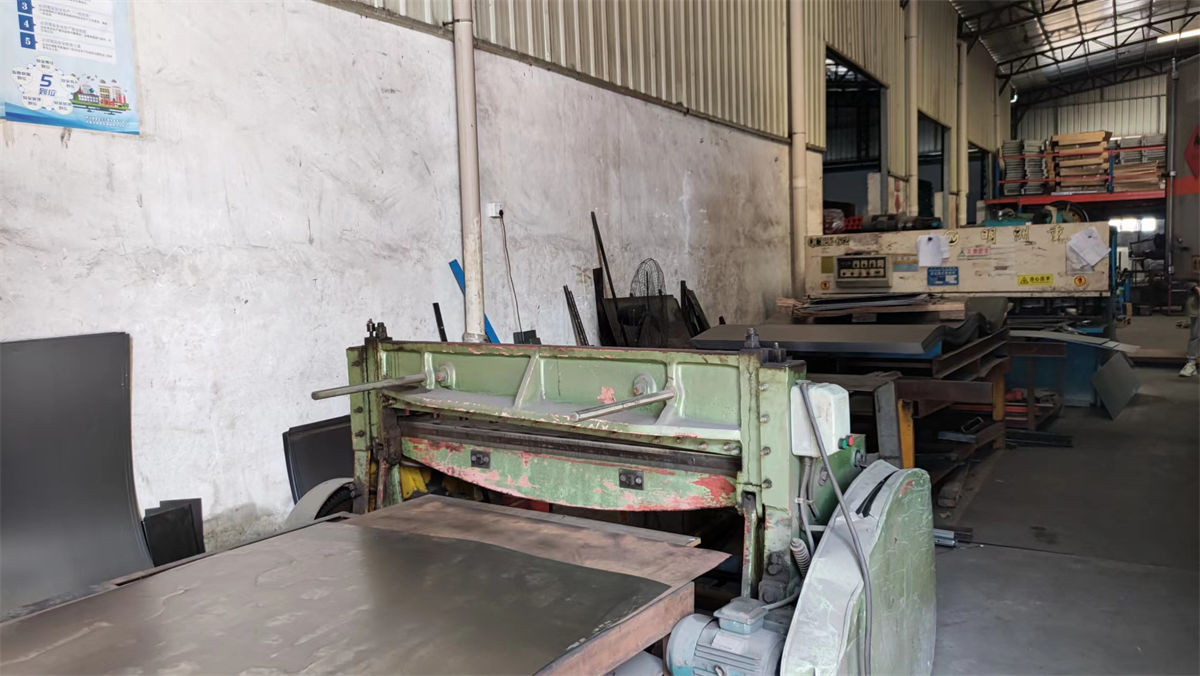
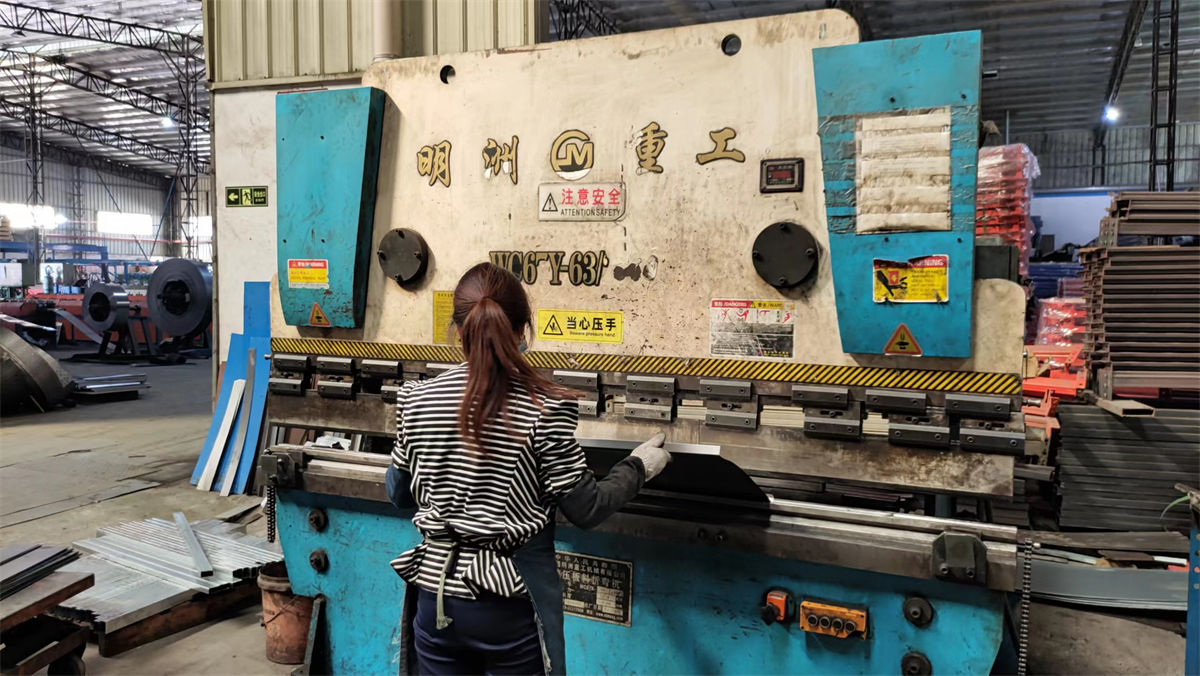
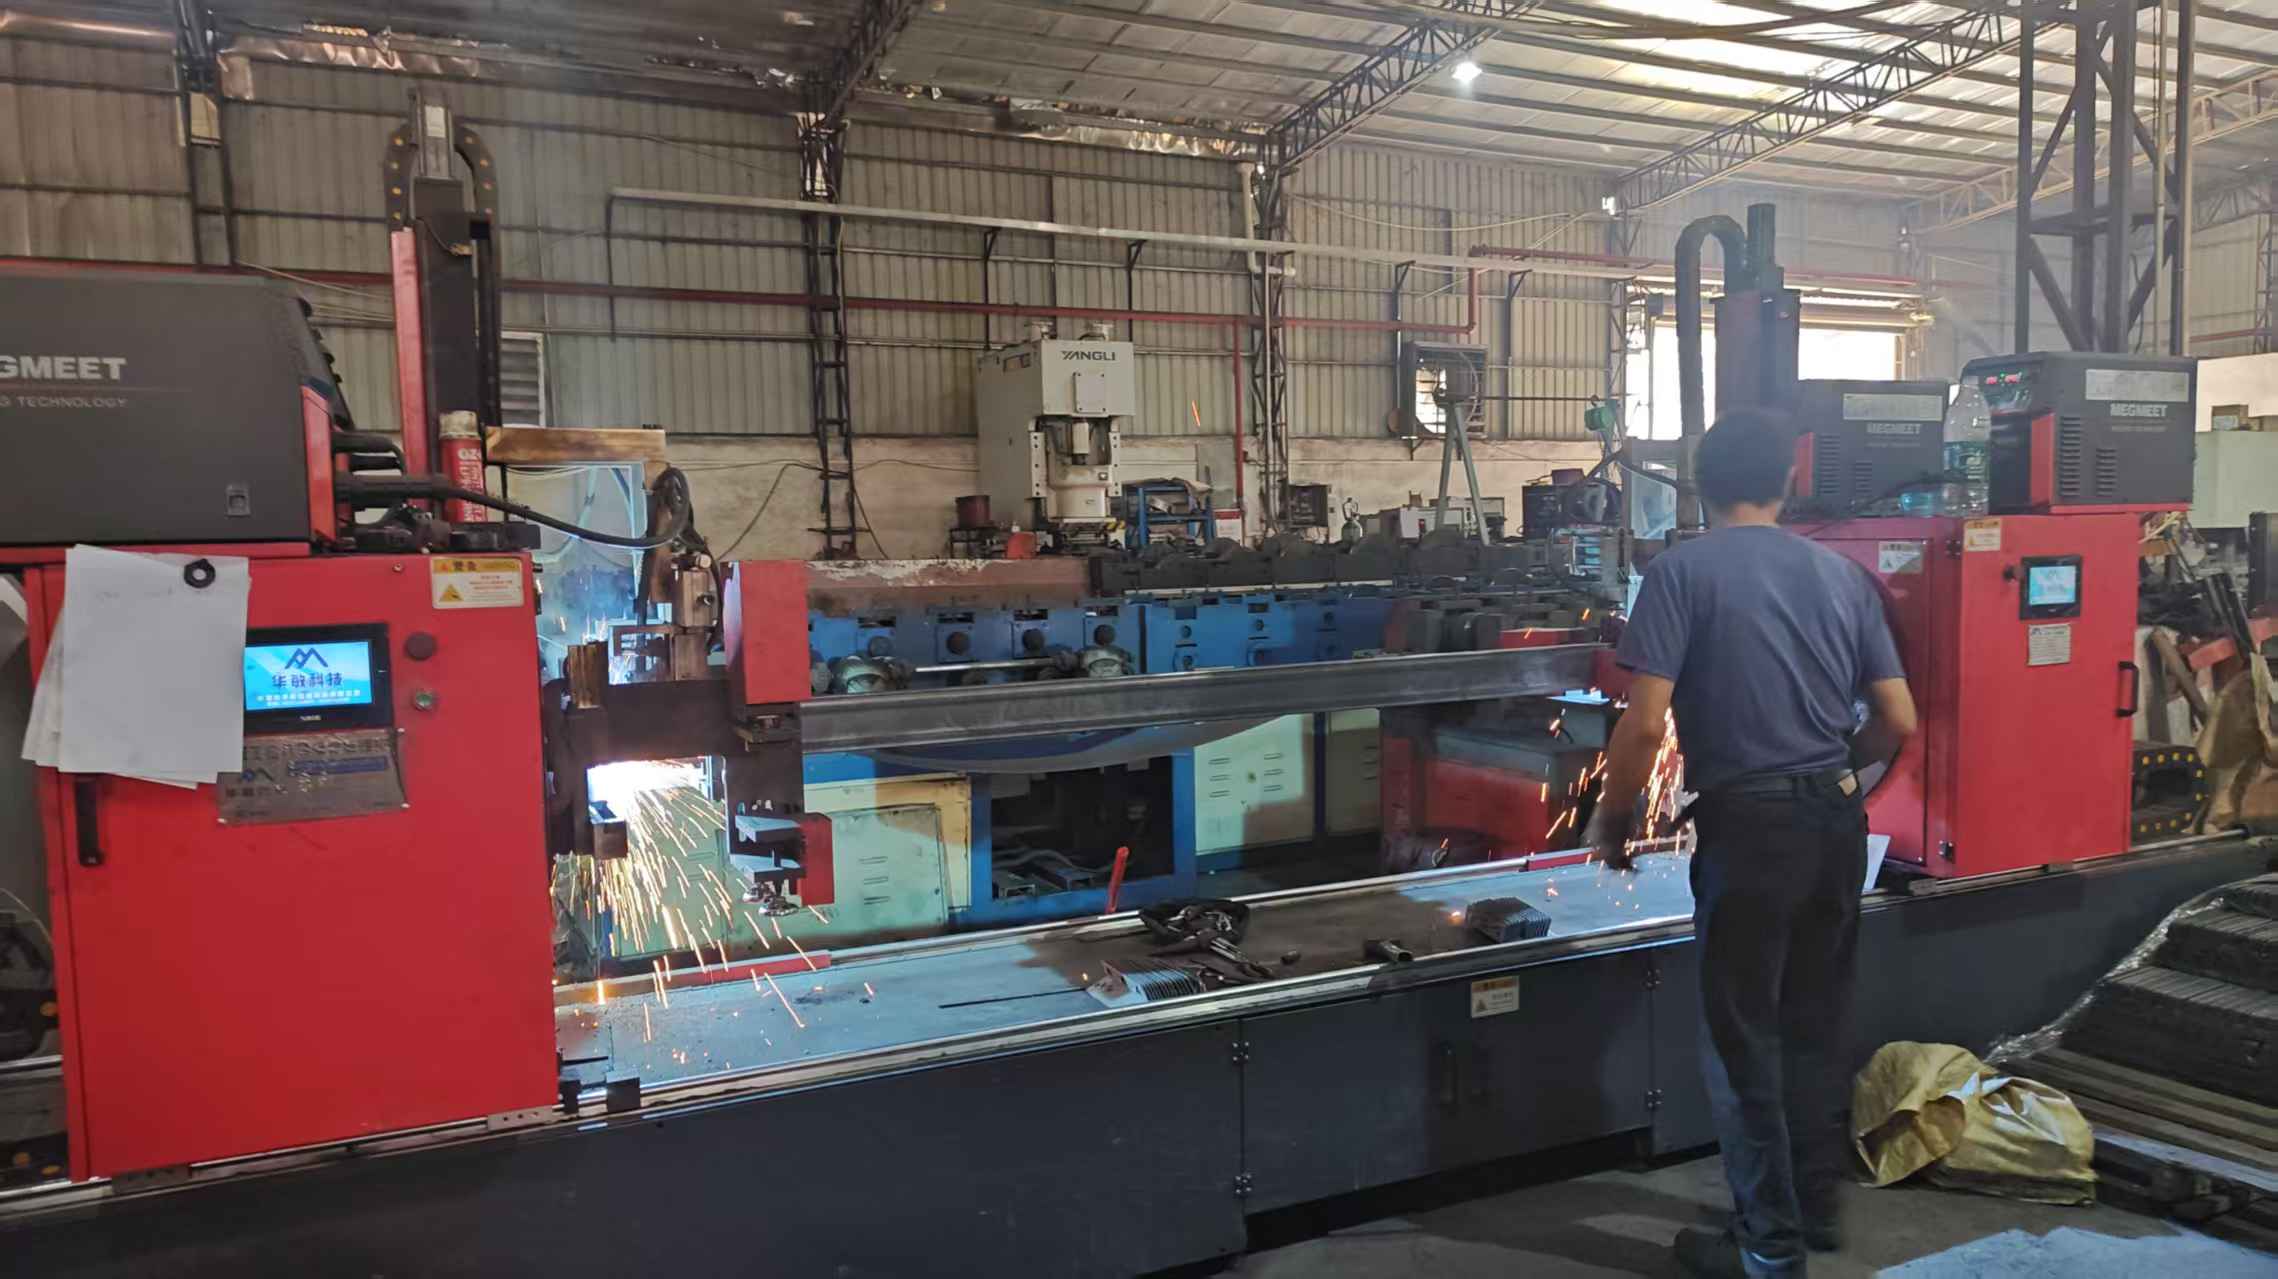
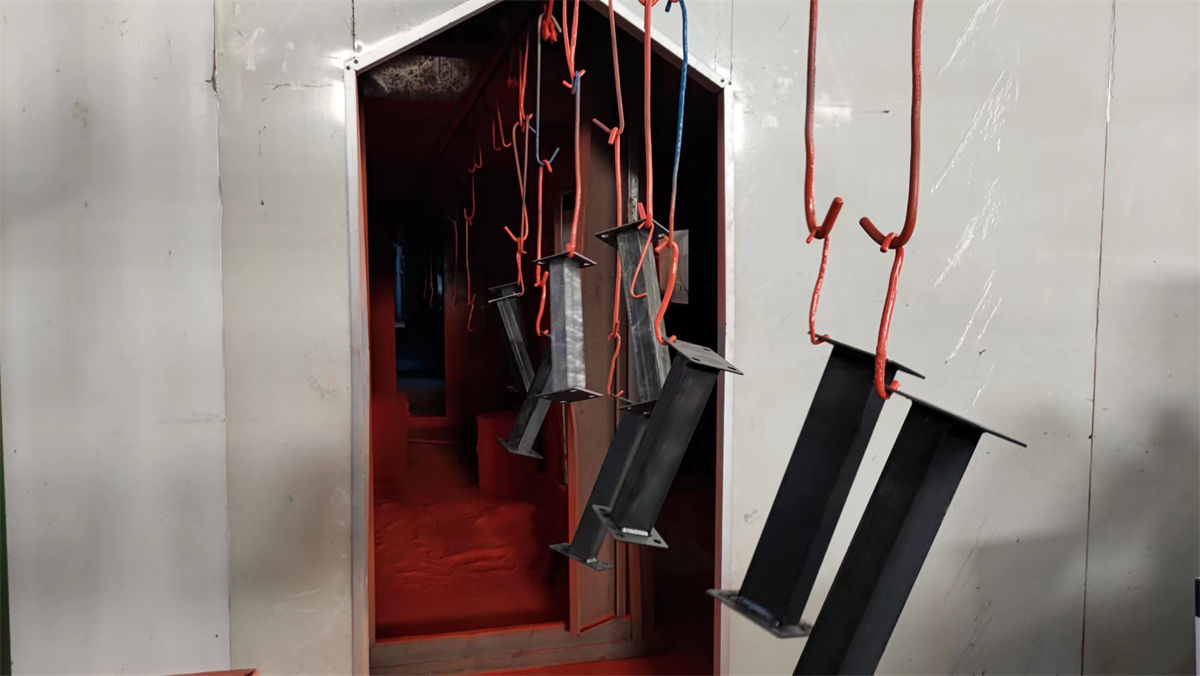
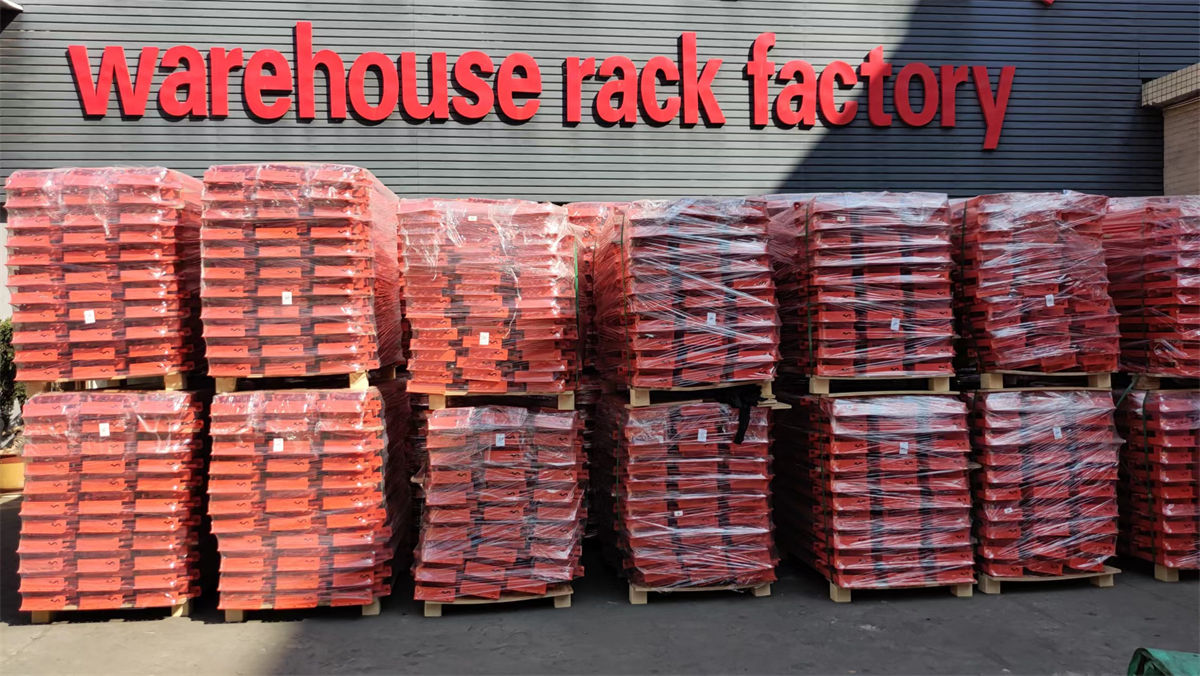
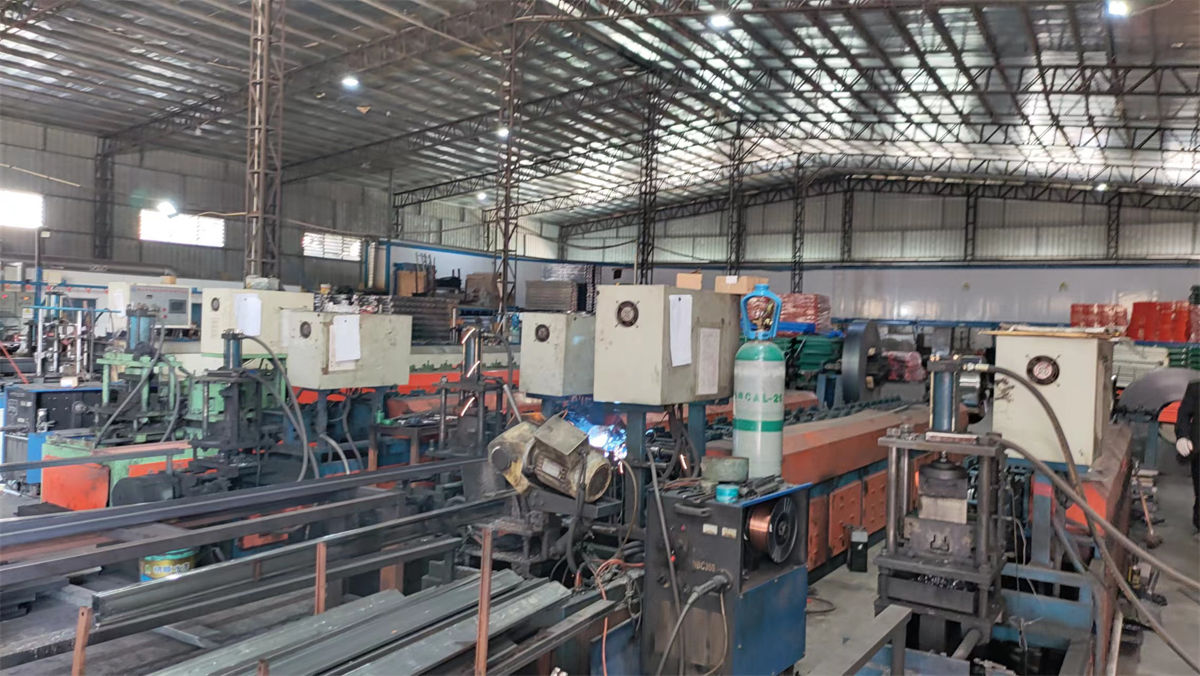
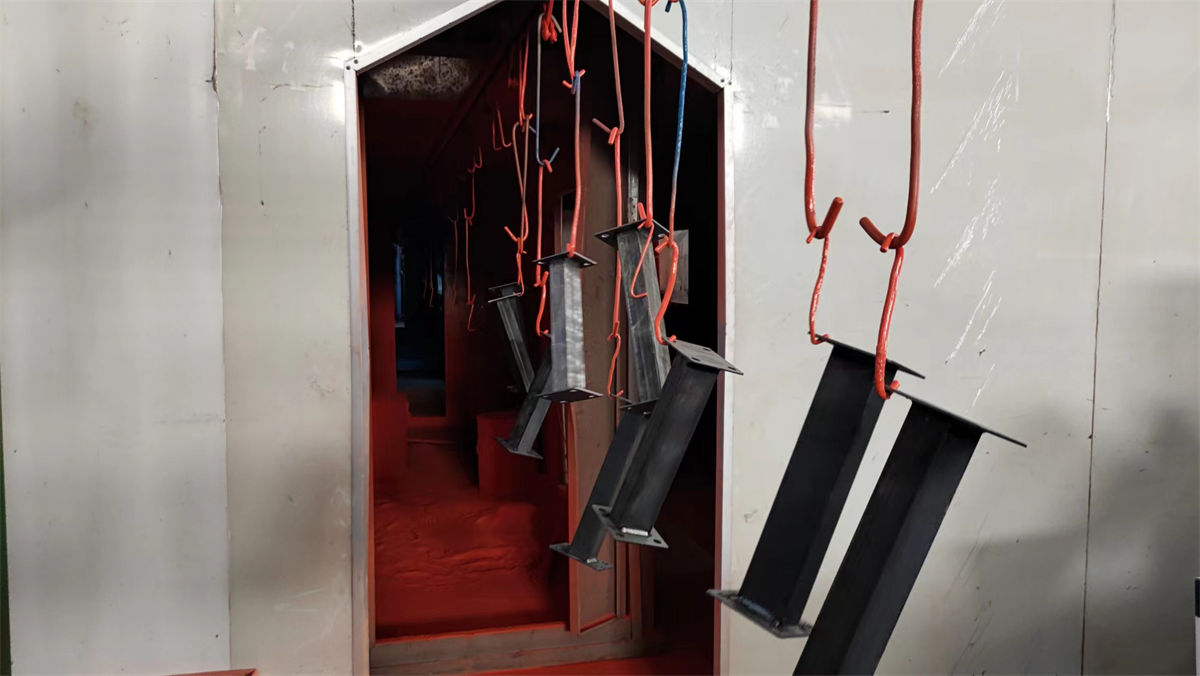
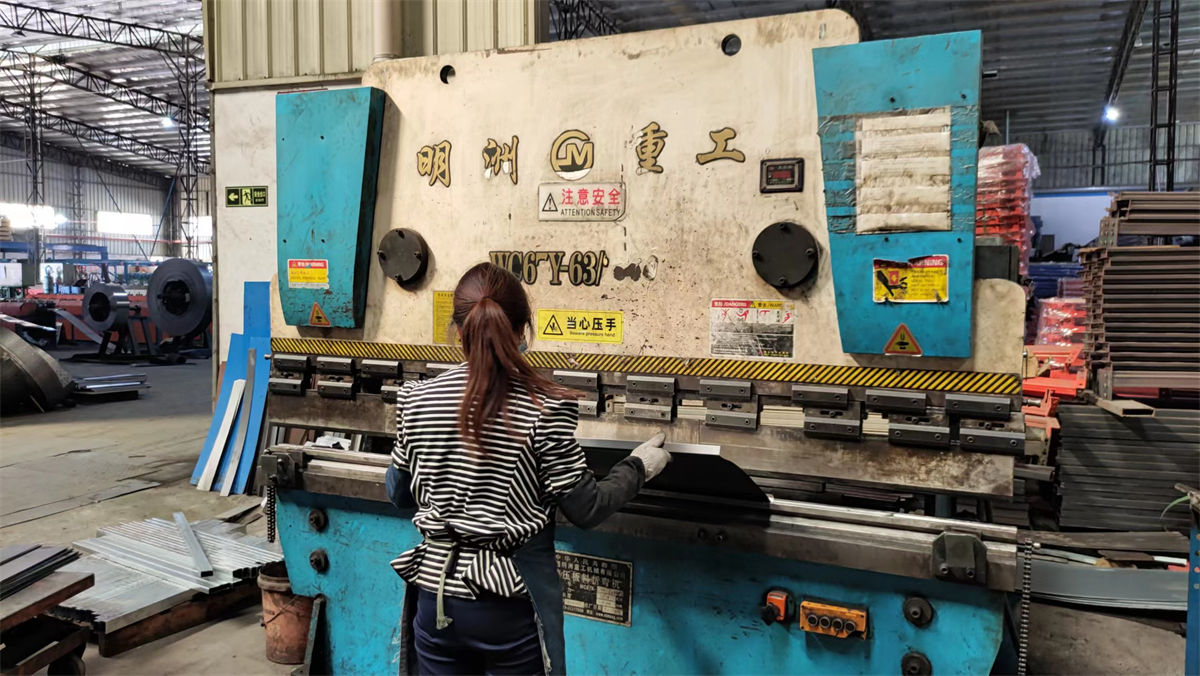
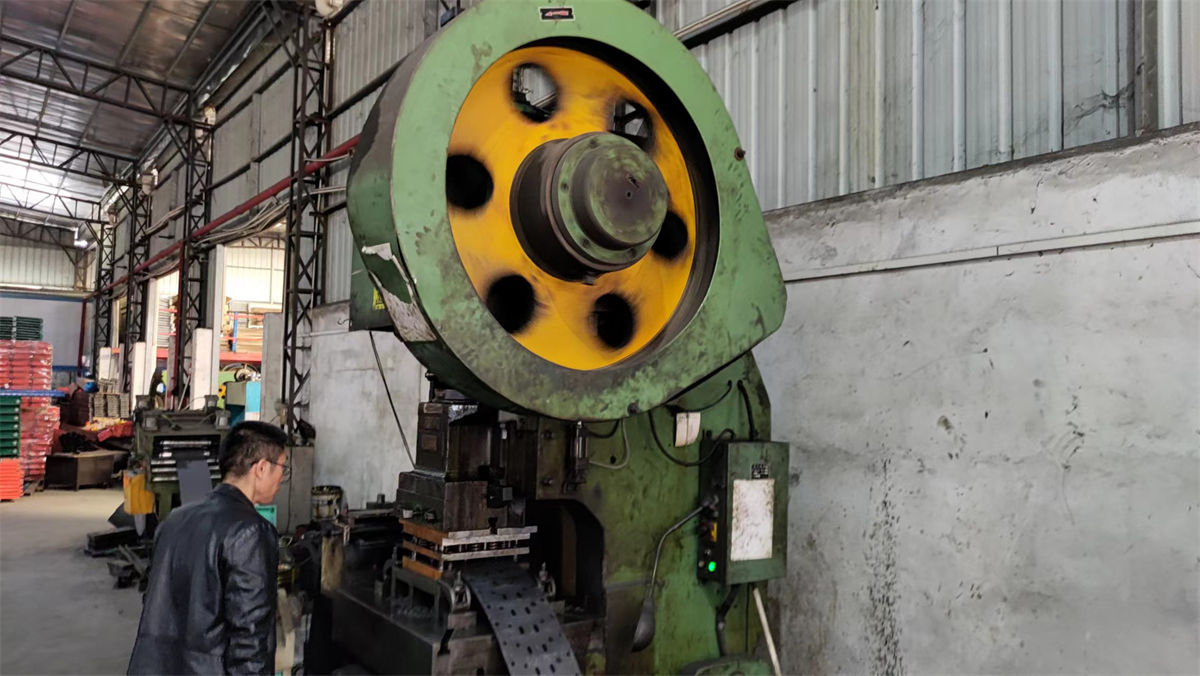
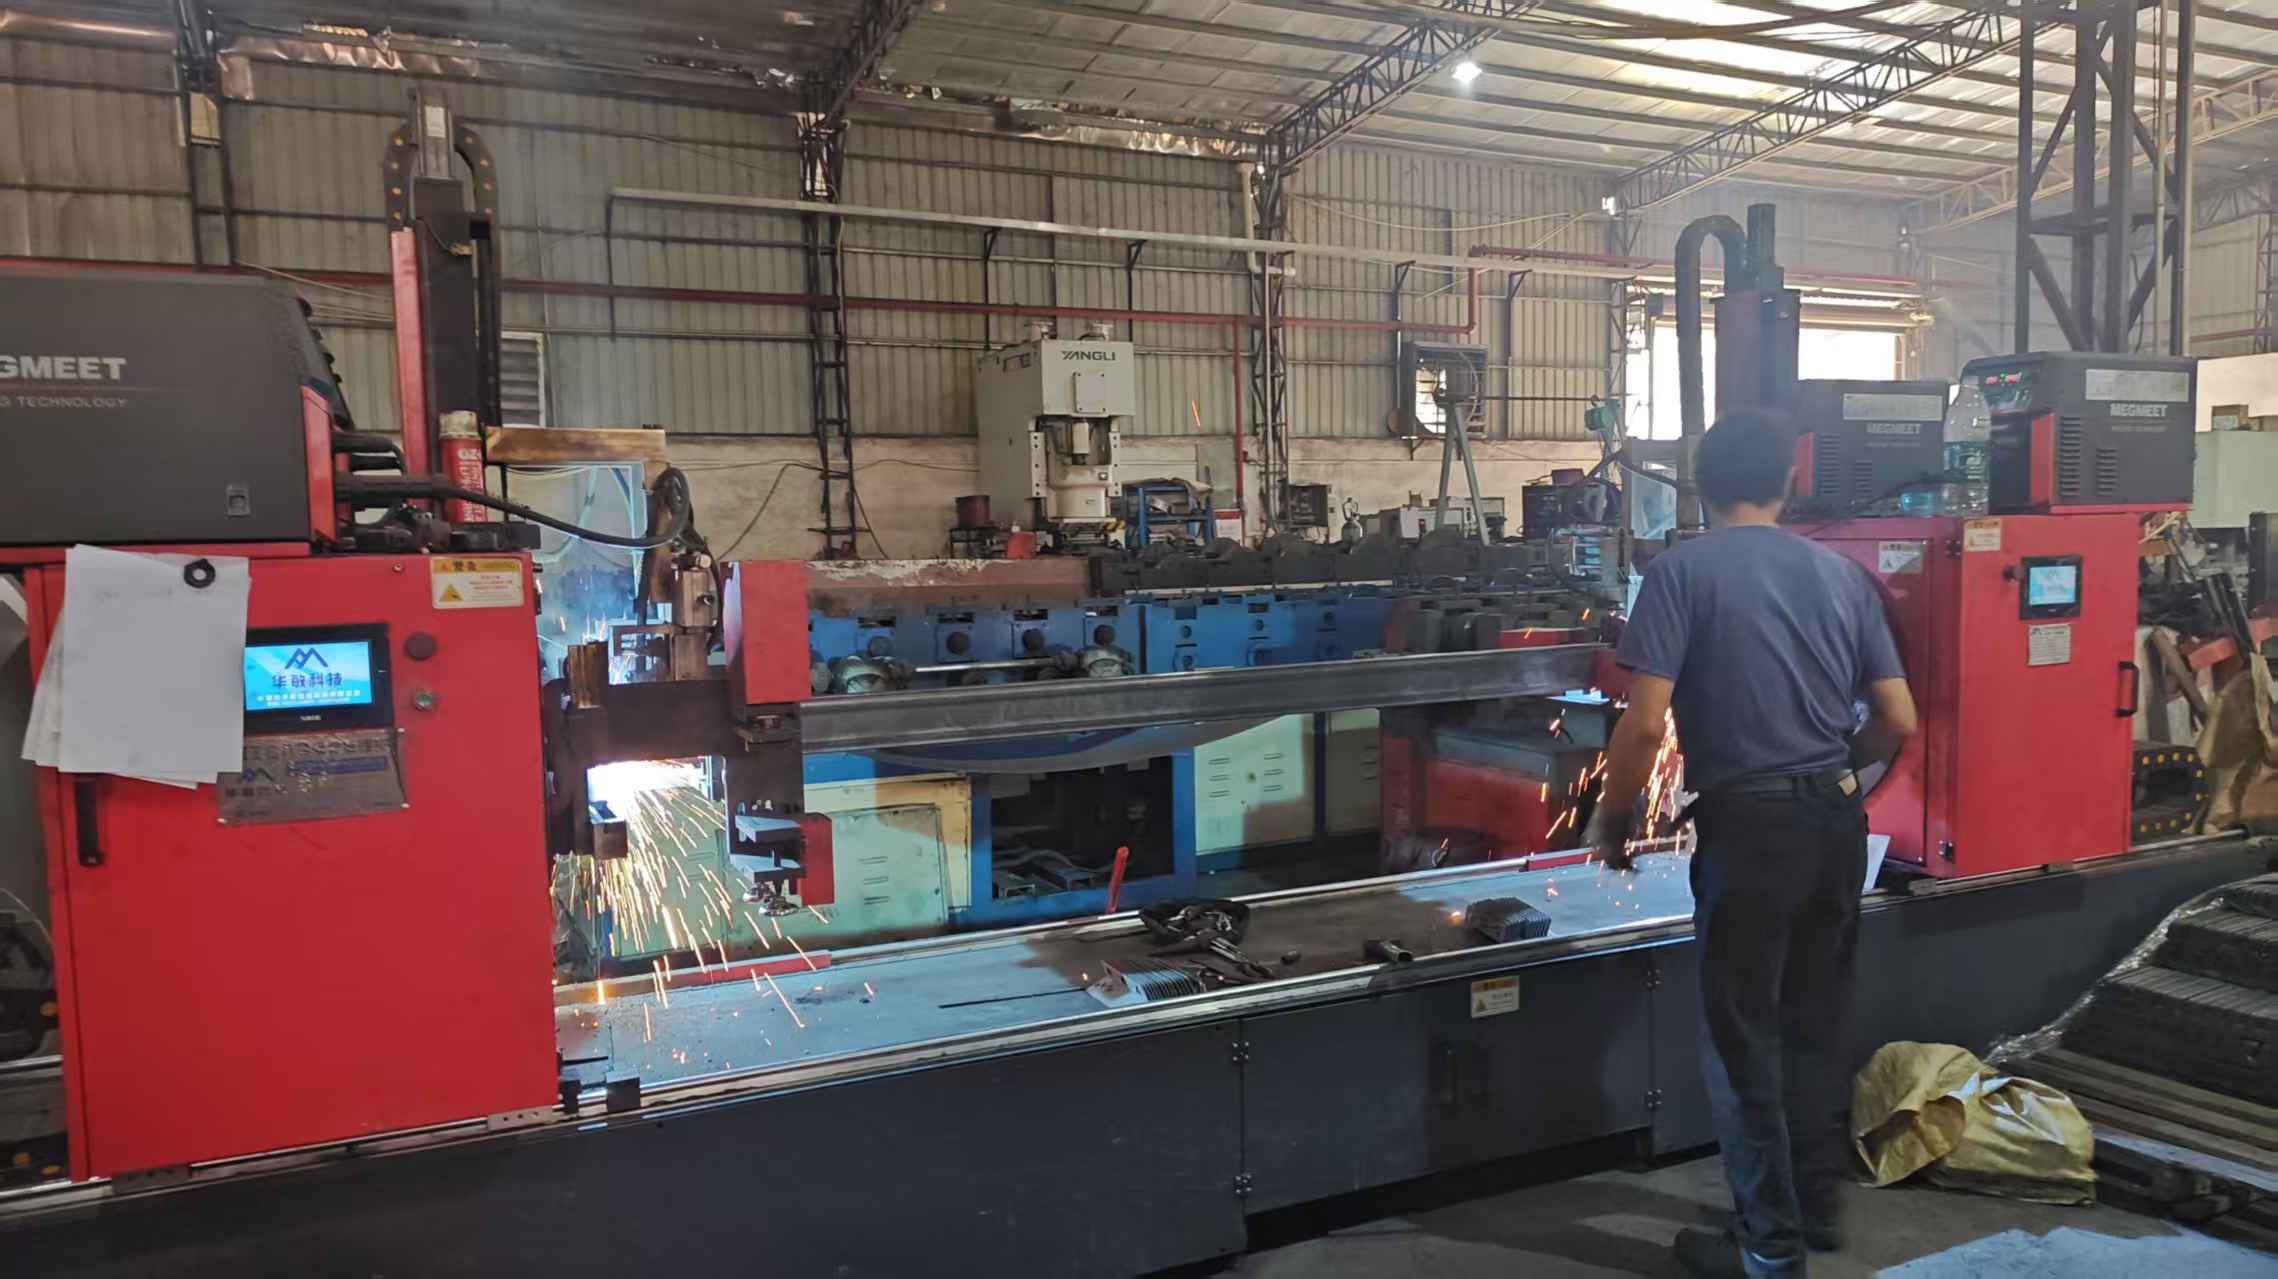
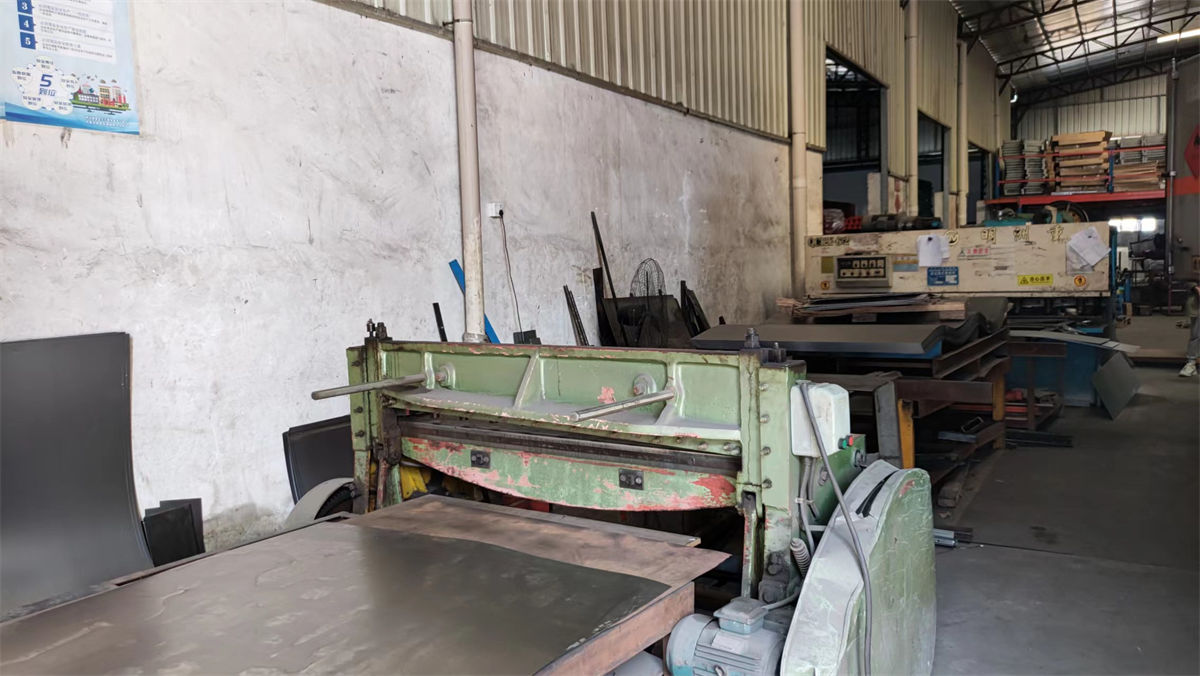
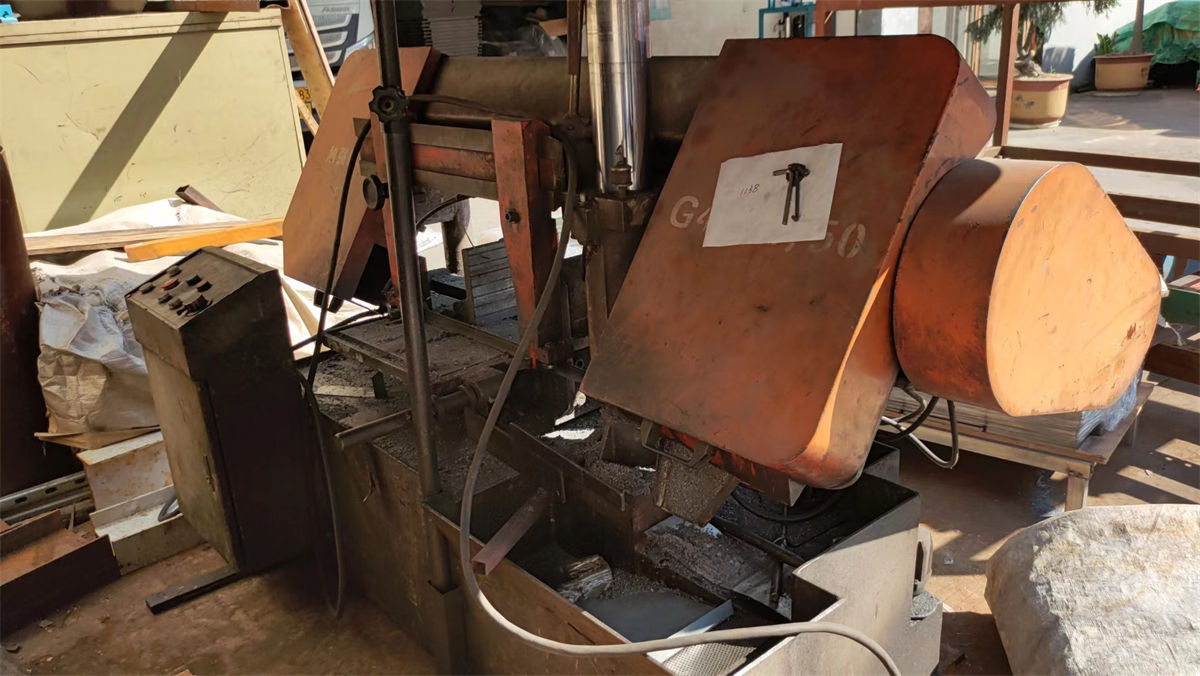
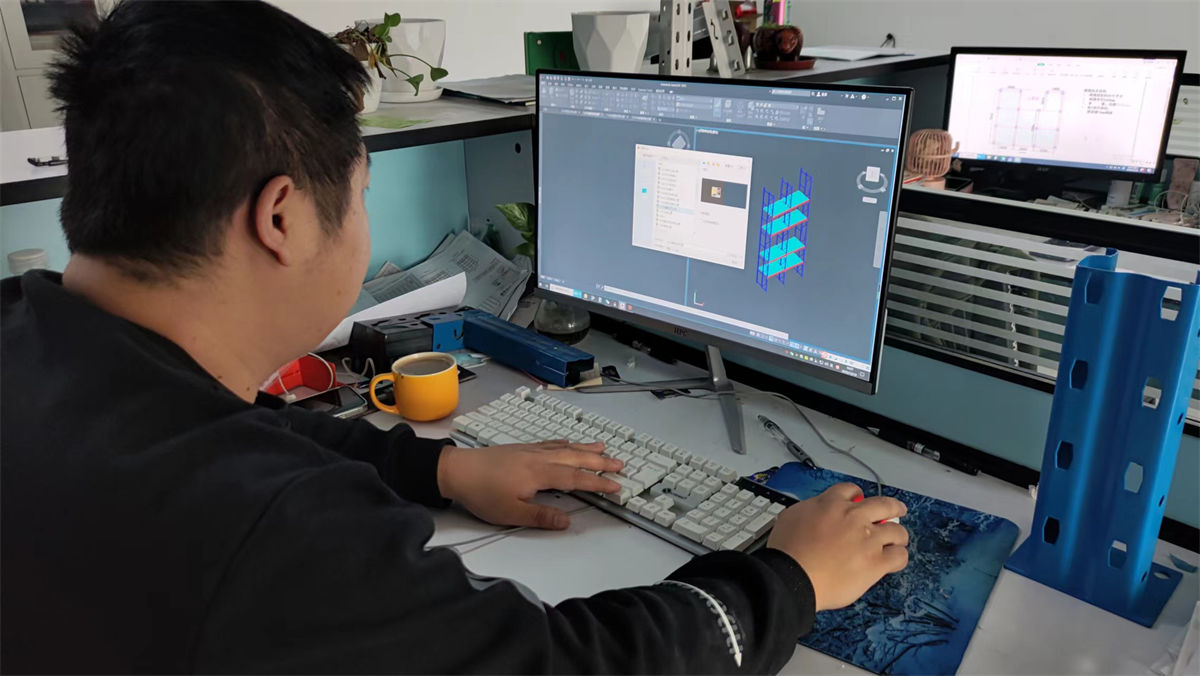
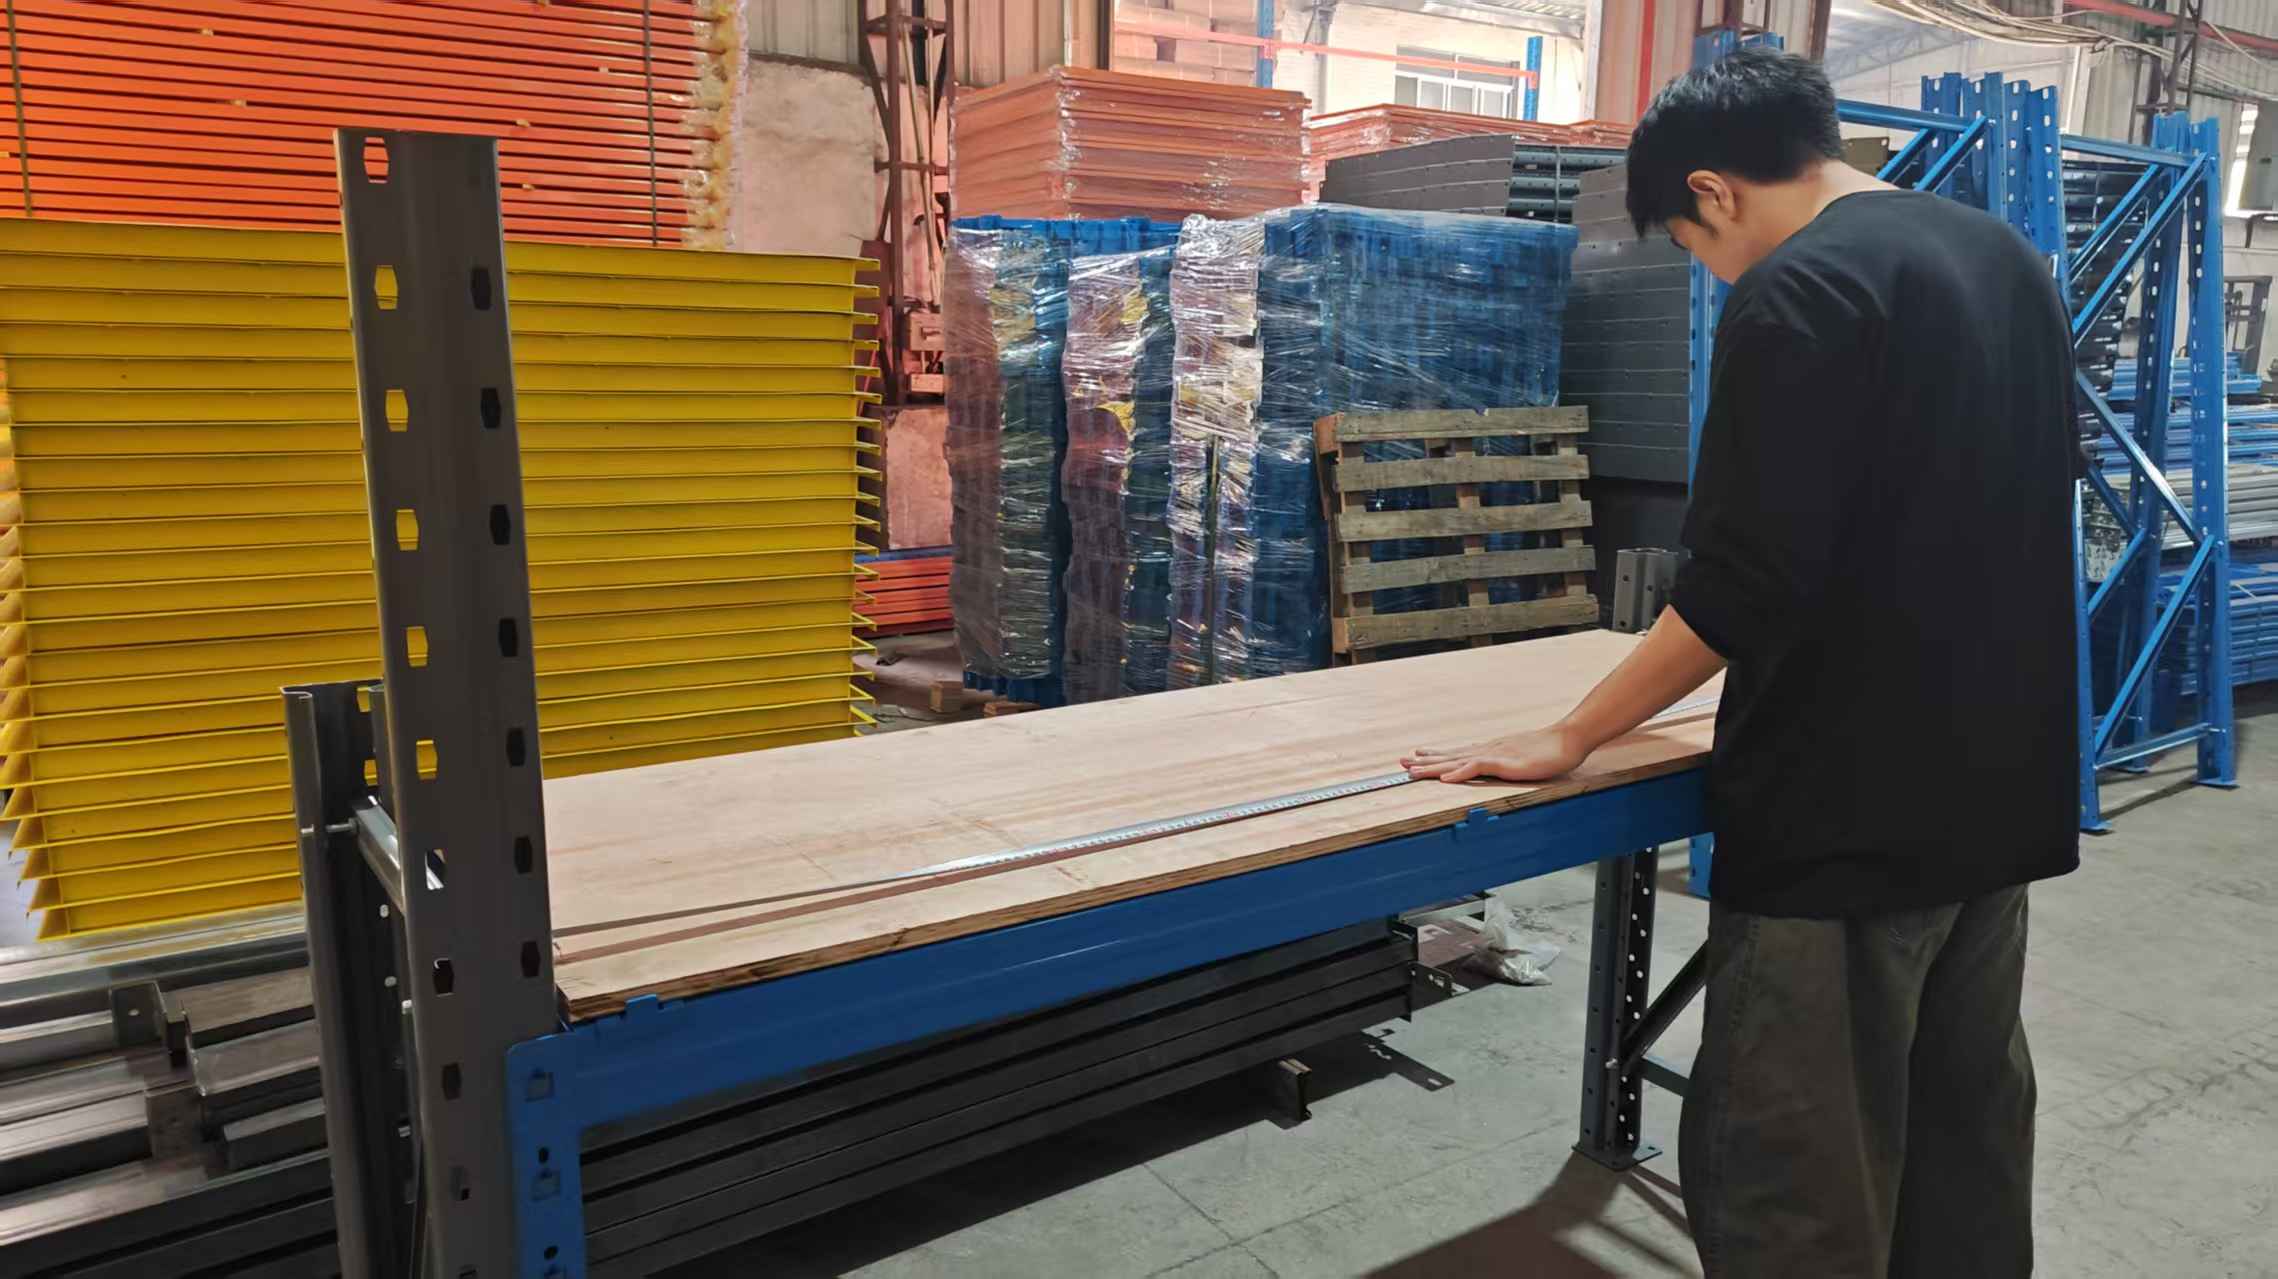
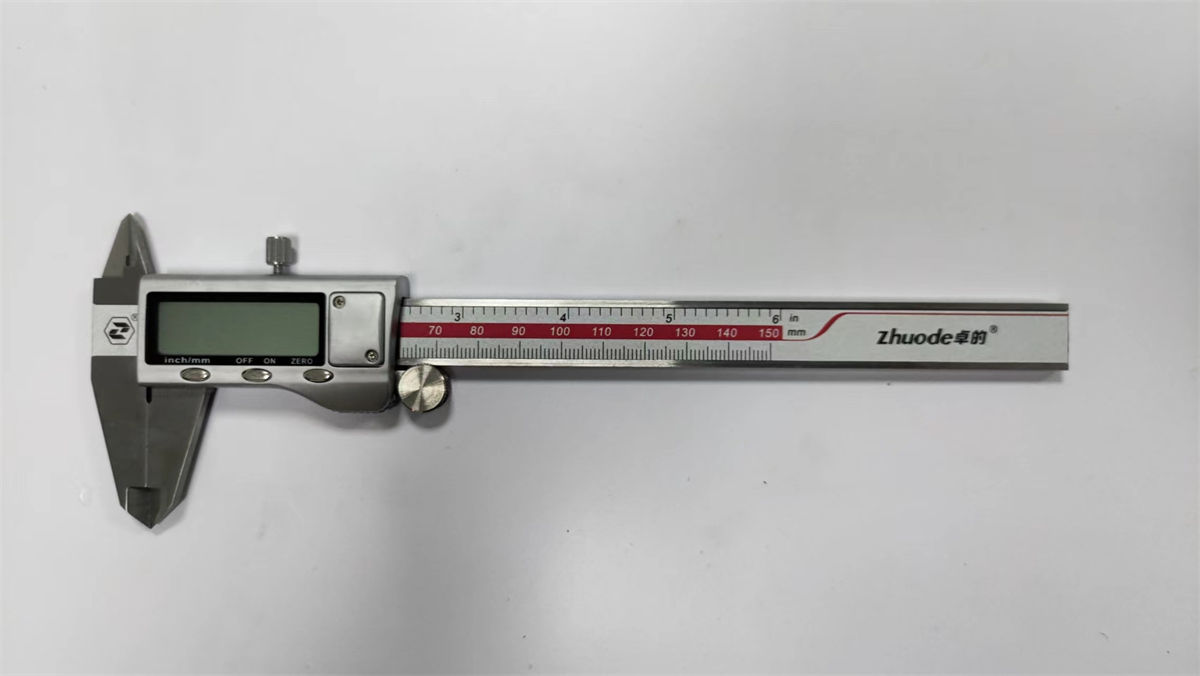
Our gravity flow racking and industrial shelving lines are manufactured strictly according to international structural standards including FEM (European Federation of Materials Handling), RMI (Rack Manufacturers Institute), and ISO9001 quality management benchmarks. Every export batch undergoes rigorous third-party load verification to ensure total structural compliance across North American, European, and Asia-Pacific markets.
Designed for diverse high-throughput sectors including food & beverage cold storage, automotive component distribution, fast-moving consumer goods (FMCG) e-commerce fulfillment, and pharmaceutical warehousing. Gravity flow systems maximize cold chain efficiency by minimizing open door times and consolidating storage footprints.

 Xinmiao Storage